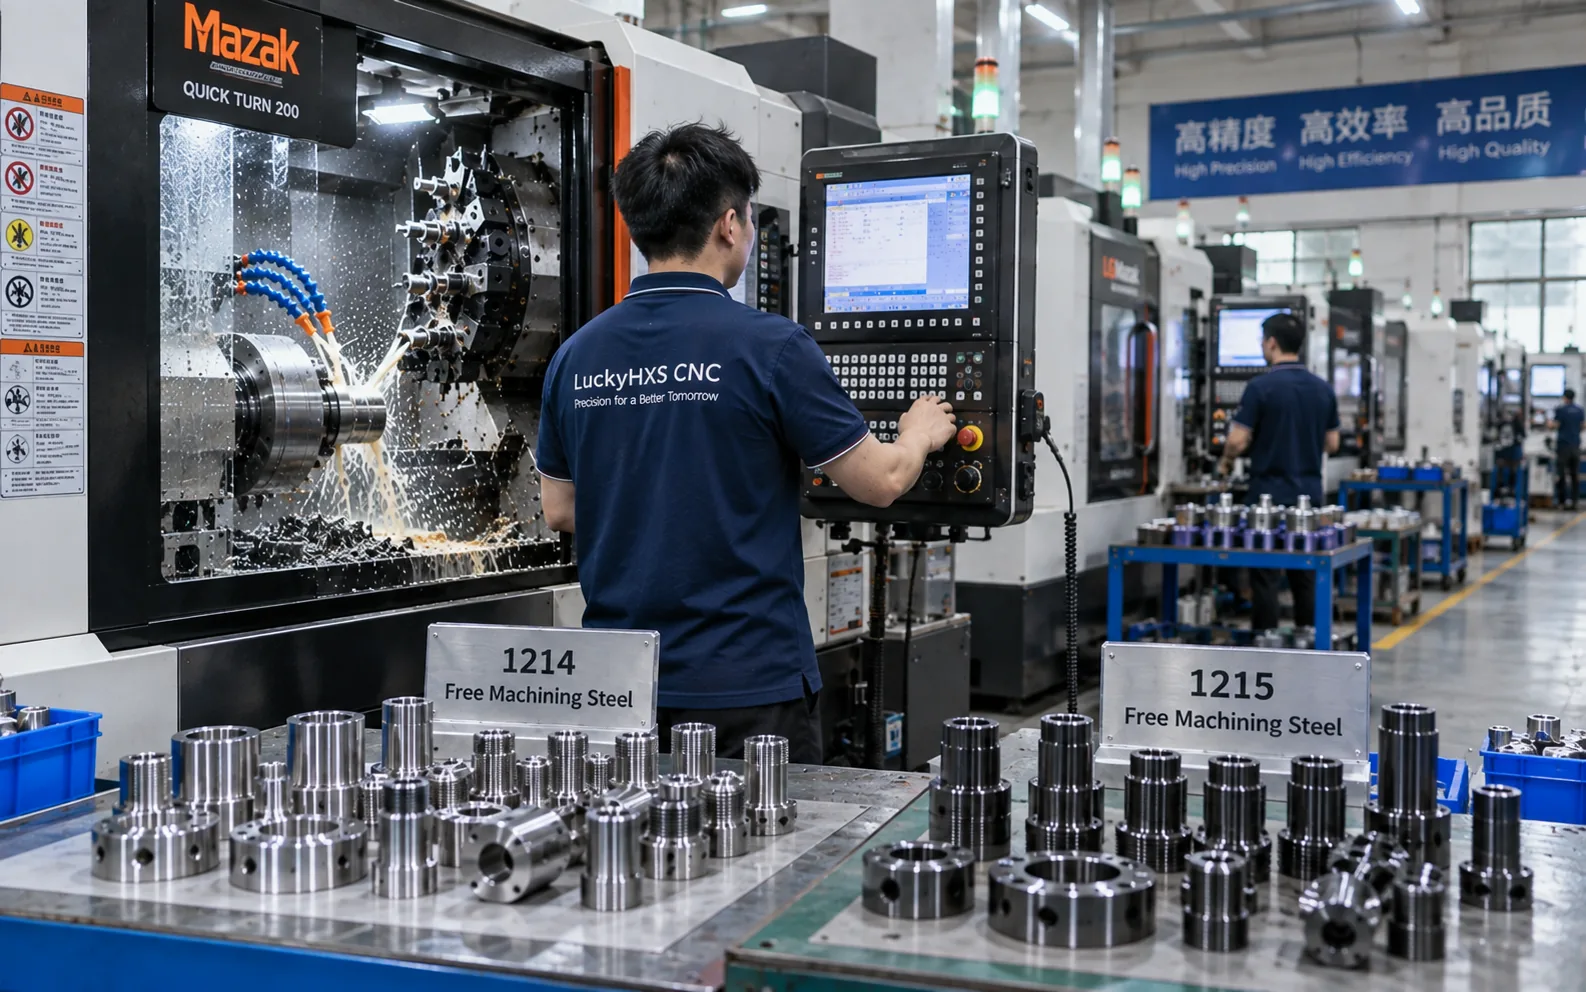
Choosing between 1214 and 1215 free-machining steel matters when a CNC part must combine fast cycle times, clean chip control, stable dimensions, and cost-efficient production. Both grades are widely used for CNC turned steel parts, Swiss machined steel parts, shafts, pins, bushings, fittings, and precision lathe components, but their sulfur and lead-related characteristics affect machinability, finish, forming behavior, and compliance decisions.
1214 vs 1215 Free-Machining Steel: Key Differences & Machinability
Free-machining steel CNC parts are precision components produced from steels engineered for easier cutting, short chips, smooth finishes, and faster cycle times. 1214 and 1215 are common choices for CNC turning and Swiss machining, especially when high productivity, tight repeatability, and economical production are more important than high strength or welding performance.
Material Definition and Typical CNC Part Forms
Free-machining steels are low-carbon steels modified with elements such as sulfur, phosphorus, and sometimes lead to improve cutting performance. These additions help chips break cleanly, reduce tool pressure, and improve surface quality during CNC lathe machining.
For 1214 and 1215, the main value is production efficiency. They are not selected for heavy structural loading, high toughness, or demanding welding. Instead, they are preferred for precision turned parts where cutting performance, dimensional stability, and repeatability are critical.
Common applications include:
- CNC turned steel parts such as spacers, collars, threaded inserts, shafts, pins, and bushings
- Swiss machined steel parts such as small connectors, precision sleeves, miniature shafts, and instrument components
- High-volume lathe parts requiring knurling, threading, grooving, drilling, and reaming
- Components that require surface finishing for free-machining steel, such as zinc plating, black oxide, nickel plating, or passivation-like protective coatings
- Low-to-medium load mechanical parts where fast production and cost control are priorities
Luckyhxs Pro Tip: When we quote free-machining steel CNC parts, we first check whether the part needs plating, welding, bending, or heat treatment. If it only needs accurate turning and a clean finish, 1215 is often the faster, cleaner production choice.
CNC Machining Process for 1214 and 1215 Steel Parts
CNC machining of 1214 and 1215 works by using their free-cutting chemistry to reduce cutting resistance, create short chips, and maintain stable tool life. In turning, drilling, threading, and Swiss machining, these steels allow high spindle speeds, consistent finishes, and efficient production of small-to-medium precision parts.
Cutting Behavior in CNC Turning and Swiss Machining
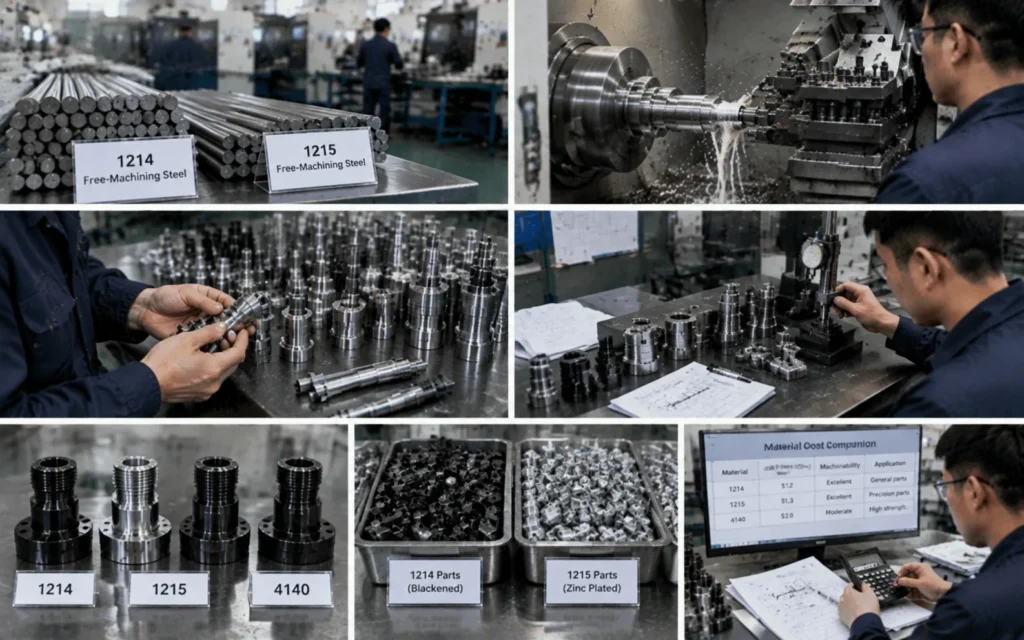
During CNC lathe machining for 1214 and 1215, the sulfur-rich inclusions in the steel act as chip breakers and internal lubricants. This improves machinability by reducing friction between the tool and workpiece. In practical production, that means faster cutting speeds, fewer chip-wrap problems, and lower risk of tool overload.
A typical machining workflow includes:
- Material selection: Choose 1214 or 1215 bar stock based on tolerance, finish, compliance, and part function.
- CNC turning setup: Use suitable inserts, tool geometry, coolant, and bar feeder settings.
- Rough turning: Remove material quickly while controlling chip evacuation.
- Finishing passes: Achieve final diameter, concentricity, grooves, shoulders, and surface finish.
- Secondary operations: Add drilling, tapping, reaming, slotting, cross holes, or milling flats.
- Surface finishing: Apply zinc plating, black oxide, phosphate, nickel plating, or oiling where corrosion resistance is needed.
- Inspection: Verify dimensions, thread gauges, runout, surface roughness, and plating thickness if required.
For Swiss machining steel parts, 1215 steel machinability is especially useful because small-diameter parts need excellent chip control. Long, stringy chips can damage surface finish or interfere with guide bushings, so free-machining grades help maintain stable unattended production.
Luckyhxs Pro Tip: In our shop experience, chip control is just as important as cutting speed. A steel that breaks chips cleanly can reduce downtime, protect the tool edge, and improve consistency across thousands of CNC turned parts.
Which steel is easiest to machine?
Among common carbon and alloy steels, 1215 is one of the easiest to machine because it is specifically designed for high-speed cutting and excellent chip control. Compared with 1214, 1215 is typically preferred for clean CNC turning, automatic screw machining, and Swiss machining when welding is not required.
Machinability Ranking for Common Production Steels
1215 is widely recognized as a benchmark free-machining steel. It generally machines more easily than 1018, 1045, 4140, and many stainless steels. Its low carbon content and free-cutting chemistry allow operators to use aggressive parameters while maintaining dimensional consistency.
Based on our internal data and market analysis, here is the breakdown:
| Steel Grade | Relative Machinability | Typical CNC Behavior | Best Use Case |
|---|---|---|---|
| 1215 | Excellent | Short chips, smooth turning, high speed capability | High-volume CNC turned and Swiss machined parts |
| 1214 | Very good | Free-cutting, stable, good for automatic machining | General precision turned parts |
| 12L14 | Excellent | Very easy cutting due to lead addition | Screw machine parts where lead is acceptable |
| 1018 | Moderate | Tougher chips, slower cutting than 1215 | Welded or formed low-carbon parts |
| 1045 | Moderate to low | Higher strength, more tool load | Shafts and stronger mechanical parts |
| 4140 | Lower than 1215 | Stronger but harder on tools | High-strength components |
| 304 Stainless | Low | Work-hardening, difficult chip control | Corrosion-resistant precision parts |
The easiest steel to machine is not always the best steel for the job. If the part requires welding, forming, high tensile strength, or fatigue resistance, a less machinable grade may be more suitable.
Luckyhxs Pro Tip: If a customer asks for the fastest machining steel, I usually start with 1215. If they also need no-lead requirements, plating performance, or restricted-substance compliance reviewed, we confirm specifications before releasing production.
What is 1215 steel equivalent to?
1215 steel is broadly comparable to free-machining low-carbon steels used in automatic turning applications, but exact equivalents depend on the standard, chemistry limits, and regional material specification. It is commonly associated with SAE/AISI 1215 and may be cross-referenced with similar sulfurized free-cutting steels in global standards.
International Reference Grades and Specification Notes
1215 is not a high-strength alloy steel. It is a resulfurized, rephosphorized free-machining carbon steel designed for excellent turning performance. When sourcing material globally, equivalency should be confirmed by chemical composition, mechanical properties, and customer drawing requirements—not only by grade name.
Based on our internal data and market analysis, here is the breakdown:
| Standard / Region | Common Reference | Relationship to 1215 | Notes |
|---|---|---|---|
| SAE / AISI | 1215 | Primary U.S. designation | Widely used for automatic screw machine and CNC turning |
| ASTM | Often supplied under bar stock specifications | Specification-dependent | Verify chemistry and mechanical requirements |
| JIS | Similar free-cutting carbon steels | Approximate only | Confirm sulfur and phosphorus limits |
| EN / DIN | Similar free-cutting steels such as 11SMn series | Approximate only | Not always a direct one-to-one equivalent |
| GB / Chinese Standards | Similar sulfurized free-cutting steels | Supplier-dependent | Mill certificate confirmation is required |
When precision CNC parts are exported, the safest approach is to request mill certificates and confirm the required standard on the drawing or purchase order. This avoids substitution errors, especially for automotive, electrical, industrial, and regulated components.
Luckyhxs Pro Tip: We do not treat “equivalent” as automatic approval. For Luckyhxs production, we compare the certificate chemistry, machining behavior, finish requirements, and customer standard before accepting a substitute material.
What are the key differences between 4140 and 1215 steel?
4140 and 1215 serve very different purposes. 1215 is chosen for fast machining, clean chip control, and economical CNC turned parts, while 4140 is selected for strength, toughness, fatigue resistance, and heat-treatable performance. If the part carries heavy load, 4140 is usually more suitable.
Strength Versus Machining Efficiency
The main difference is design intent. 1215 is optimized for machinability. 4140 is a chromium-molybdenum alloy steel optimized for mechanical performance. This affects production cost, tool wear, finishing options, and end-use suitability.
Based on our internal data and market analysis, here is the breakdown:
| Factor | 1215 Free-Machining Steel | 4140 Alloy Steel |
|---|---|---|
| Main purpose | Fast CNC machining | High strength and toughness |
| Carbon level | Low carbon | Medium carbon alloy |
| Alloying elements | Sulfur and phosphorus for machinability | Chromium and molybdenum for strength |
| Machinability | Excellent | Moderate |
| Heat treatment | Limited strengthening potential | Excellent heat-treat response |
| Weldability | Poor to limited | Better than 1215 but requires control |
| Typical parts | Pins, spacers, fittings, bushings, inserts | Shafts, gears, couplings, bolts, tooling parts |
| Cost per machined part | Often lower for turned components | Higher due to slower machining and tooling load |
For simple precision parts, 1215 can reduce machining time significantly. For power transmission, dynamic loading, impact, or fatigue-critical applications, 4140 is usually the safer engineering material.
Luckyhxs Pro Tip: I never recommend replacing 4140 with 1215 just to reduce machining cost unless the engineering load case is reviewed. Machinability savings are not worth a field failure.
Key Features & Comparison
1214 and 1215 are both free-machining steels, but 1215 generally offers better machinability, chip control, and productivity for CNC turning. 1214 remains useful for general automatic machining, while 1215 is often preferred for high-volume precision parts where clean cutting and consistent surface finish are key priorities.
Practical Comparison for CNC Machined Components
Based on our internal data and market analysis, here is the breakdown:
| Feature | 1214 Steel | 1215 Steel | Practical Meaning for CNC Parts |
|---|---|---|---|
| Material type | Free-machining low-carbon steel | Free-machining low-carbon steel | Both are suitable for economical turned parts |
| Machinability | Very good | Excellent | 1215 usually supports faster, cleaner production |
| Chip control | Good | Better | 1215 helps reduce chip wrapping in CNC and Swiss machining |
| Surface finish after turning | Good | Very good | 1215 can produce cleaner finishes with stable tooling |
| Strength | Low to moderate | Low to moderate | Neither is ideal for high-load structural parts |
| Weldability | Poor to limited | Poor to limited | Avoid if welding is a major requirement |
| Formability | Limited compared with mild steel | Limited compared with mild steel | Not the best choice for severe bending or forming |
| Threading performance | Good | Excellent | 1215 is strong for threaded inserts and precision screw-machine parts |
| Plating compatibility | Good with proper cleaning | Good with proper cleaning | Surface preparation is critical before zinc, nickel, or black oxide |
| Typical production method | CNC turning, automatic machining | CNC turning, Swiss machining, screw machining | 1215 is common in high-volume bar-fed production |
| Typical applications | Bushings, collars, fittings, spacers | Pins, shafts, inserts, fittings, precision small parts | Selection depends on tolerance, finish, and volume |
| Cost efficiency | Good | Very good in high-volume turning | Faster cycle time can reduce total part cost |
When comparing 1214 steel vs 1215 steel, the most important factor is not only raw material price. The real difference often appears in cycle time, tool life, scrap rate, and the ability to keep production stable over long runs.
Luckyhxs Pro Tip: For long-running CNC lathe jobs, I focus on total machining cost rather than bar stock price. If 1215 shortens cycle time and reduces tool changes, it can be the better value even if the material quote is slightly higher.
Cost & Buying Factors
The cost of 1214 and 1215 CNC parts depends on material availability, part geometry, tolerance, production volume, surface finishing, and inspection requirements. 1215 often lowers total machining cost in high-volume turning because its excellent machinability can reduce cycle time, tool wear, and downtime.
What Drives the Final CNC Part Price
For free-machining steel CNC parts, the quoted unit price is influenced by both material and manufacturing complexity. A simple spacer may be inexpensive, while a small Swiss machined part with cross holes, fine threads, plating, and tight concentricity can cost much more.
Key buying factors include:
- Material grade: Confirm whether 1214, 1215, or another free-machining steel is specified.
- Part diameter and length: Bar size affects raw material cost and machining strategy.
- Tolerance requirements: Tight tolerances require slower finishing passes and more inspection.
- Surface roughness: Fine finishes may need optimized tooling or secondary polishing.
- Threading and holes: Internal threads, deep holes, cross holes, and micro features increase cycle time.
- Surface finishing: Zinc plating, black oxide, nickel plating, phosphate, and oiling add cost and lead time.
- Order quantity: Higher volume spreads setup cost across more parts.
- Inspection level: Full dimensional reports, PPAP, material certificates, and plating reports affect pricing.
- Packaging requirements: Anti-rust packaging, separated cavities, and export packaging may be necessary for finished parts.
A well-prepared RFQ should include a 2D drawing, 3D model, material grade, finish requirement, tolerance standard, annual quantity, and any compliance requirements such as RoHS, REACH, or customer-specific specifications.
Luckyhxs Pro Tip: The fastest way to reduce cost is to review tolerances. If only one feature needs ±0.01 mm, do not apply that tolerance to the entire drawing. Selective tolerancing keeps CNC turned steel parts accurate and economical.
Conclusion
1214 and 1215 are both practical choices for precision free-machining steel components, but 1215 is usually the stronger option for high-speed CNC turning and Swiss machining. The best selection depends on machinability, finishing needs, compliance, tolerances, load requirements, and total production cost.
Final Selection Guidance for Buyers and Engineers
For most CNC turned steel parts where machining efficiency is the priority, 1215 is often the preferred material. It provides excellent chip control, reliable surface finish, and strong productivity in bar-fed CNC lathes and Swiss machines. 1214 remains a useful option for general free-machining applications, especially when it is already approved by drawing or customer specification.
Before placing an order, review these points:
- Choose 1215 for high-volume CNC turning, clean chip control, and excellent machinability.
- Choose 1214 when it meets the drawing requirement and the application does not justify switching grades.
- Avoid both grades for heavily welded, highly loaded, or impact-critical parts.
- Confirm surface finishing requirements before production, especially for plated free-machining steel parts.
- Use certified material and controlled inspection when parts are used in assemblies, instruments, automotive systems, or export products.
Luckyhxs can support material selection, CNC lathe machining for 1214 and 1215, Swiss machining, secondary processing, finishing, and inspection for precision steel components.
Luckyhxs Pro Tip: If you are unsure whether 1214 or 1215 is right for your part, send the drawing and application details. I would review the tolerance, load, finish, and production volume first, then recommend the grade that gives the best balance of performance and cost.