
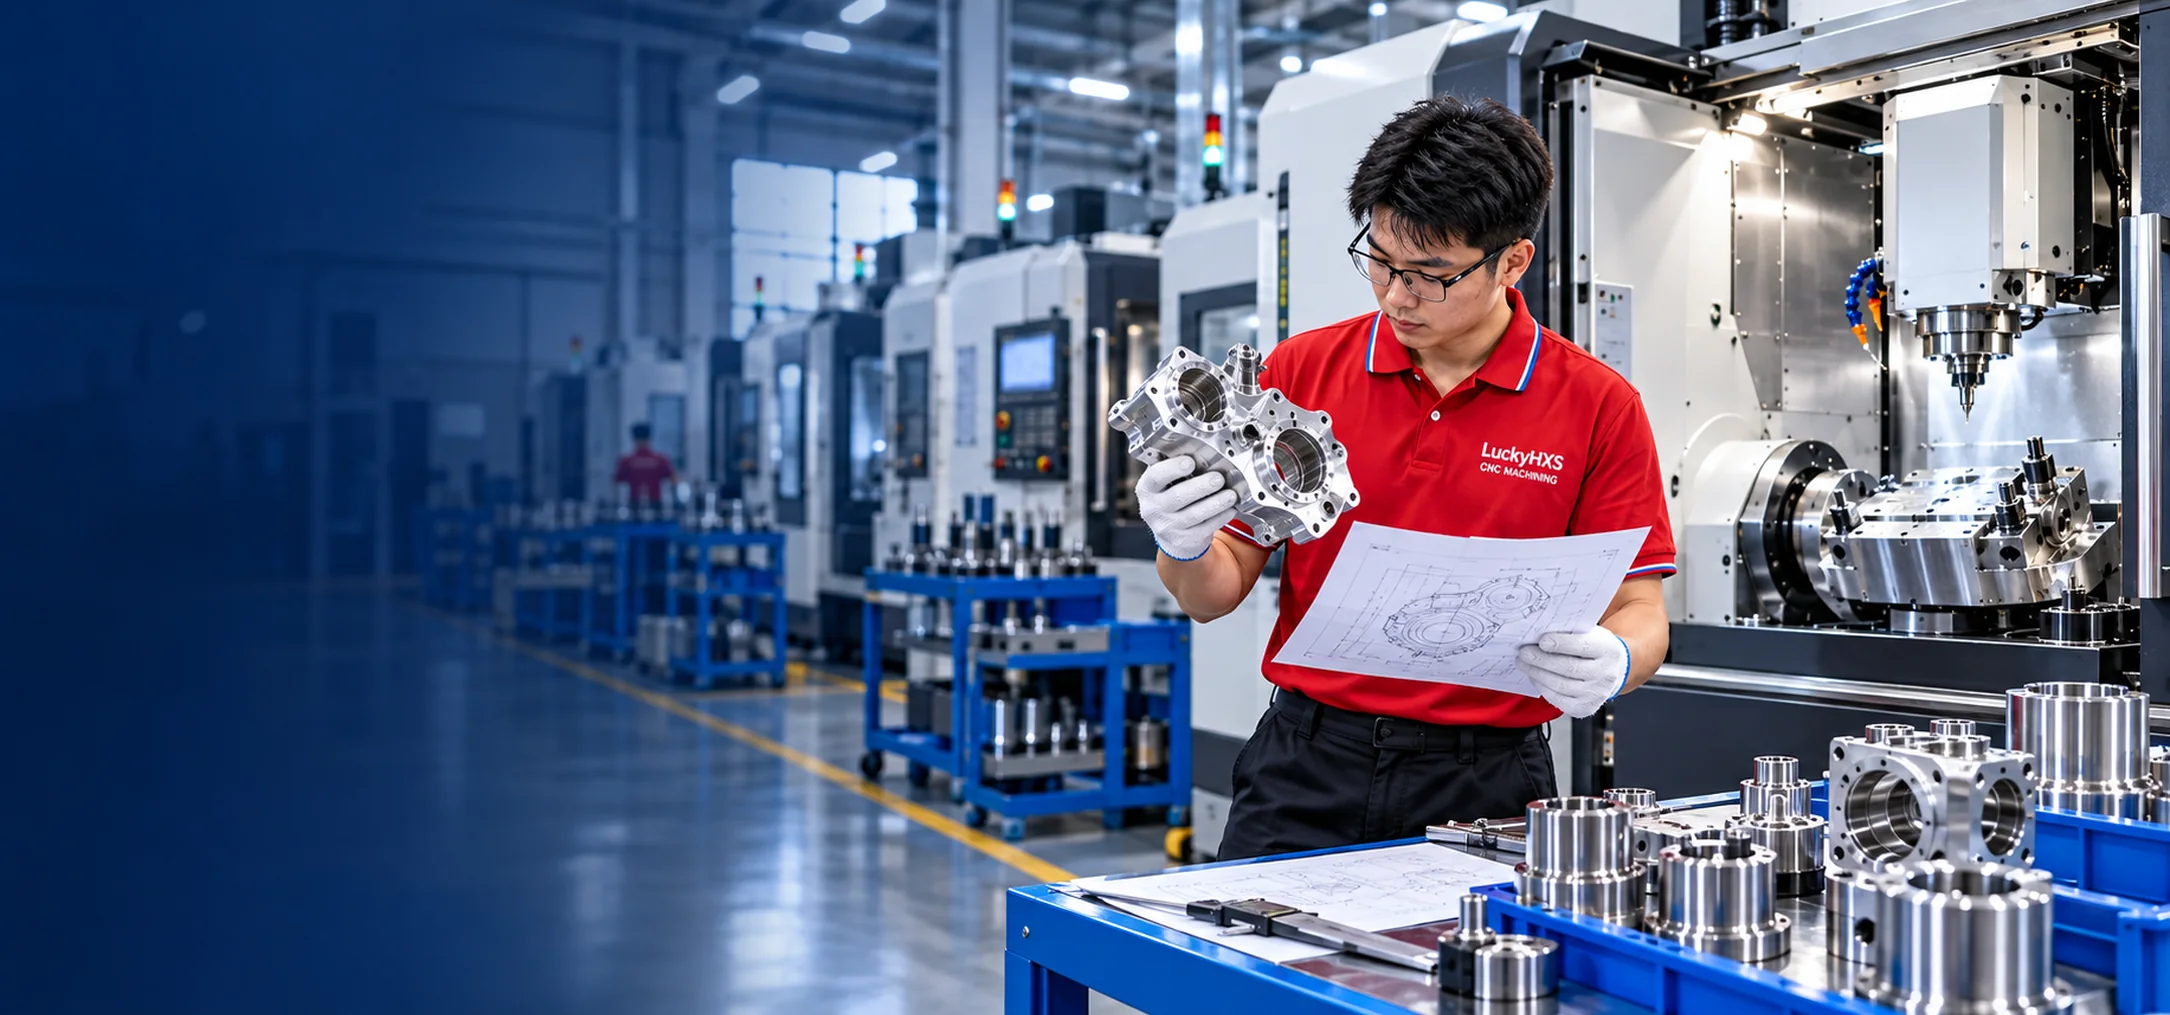
Precision CNC Milling Services Manufacturer for Custom CNC Milled Parts
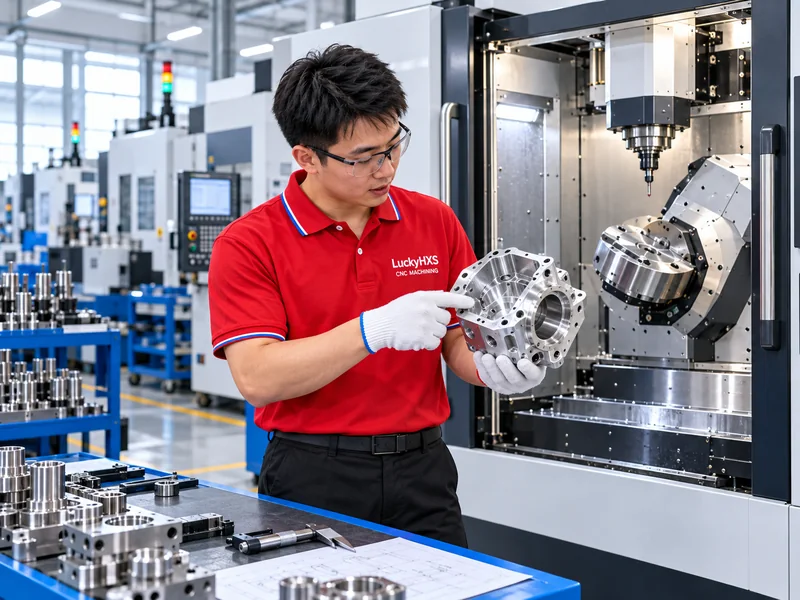
LuckyHXS manufactures precision CNC milled parts from customer drawings, 3D CAD files and approved samples. We produce housings, brackets, enclosures, plates, manifolds, fixtures and complex structural components for prototypes, low-volume programs and repeat production.
- 3-axis, 4-axis and selected 5-axis CNC milling
- Drilling, tapping, boring, pocketing, slotting and multi-face machining
- Engineering review for datums, hole positions, flatness, thin walls and critical fits
A Controlled Route from CNC Drawing to Finished Part

20+ Years CNC Experience
Drawing-based precision machining experience for custom industrial components.
153 Precision Machines
Machining resources for different materials, geometries and production quantities.
Prototype to Repeat Production
Suitable projects can move from a first sample to stable repeat manufacturing after approval.
Inspection Around Critical Features
Inspection planning focuses on datums, hole patterns, flatness, threads, surface finish and assembly fit.
Actual tolerance, timing and process selection depend on part geometry, material, quantity, finish and inspection requirements.
What Are Precision CNC Milling Services?
Precision CNC milling uses rotating cutting tools controlled by a CNC program to remove material from a metal or engineering-plastic workpiece. Unlike turning, CNC milling is suitable for parts with flat surfaces, pockets, slots, angled faces, mounting holes, threaded holes, sealing surfaces and multi-side features.
The machining route should be planned around the functional geometry. Datum structure, workholding, tool access, wall thickness, tolerance direction, surface finish and inspection method all influence the final result.
Custom CNC Milled Components for Different Assemblies
Each product family is manufactured to a drawing or approved sample. Choose the geometry closest to your project or submit the complete design for review.
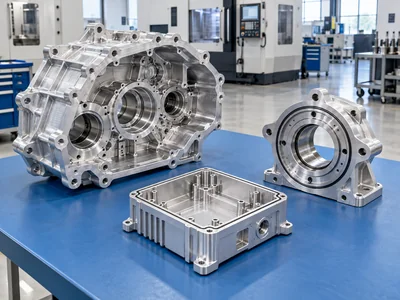
CNC Milled Housings
Internal cavities, mounting faces, connector openings and sealing surfaces for electronics, sensors and equipment.
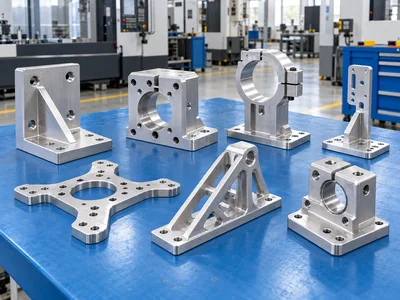
CNC Brackets and Mounts
Hole patterns, slots, datum faces and rigid mounting features for automation, robotics and machinery.

Machined Enclosures
Removable covers, cable openings, internal mounting points and controlled cosmetic surfaces.
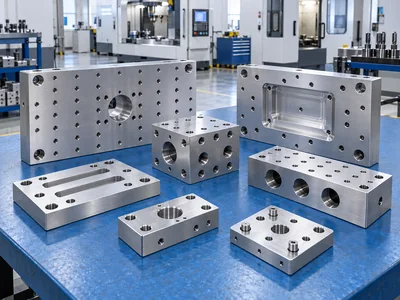
CNC Plates and Base Blocks
Flat reference faces, locating holes, pockets and mounting patterns for assemblies and fixtures.
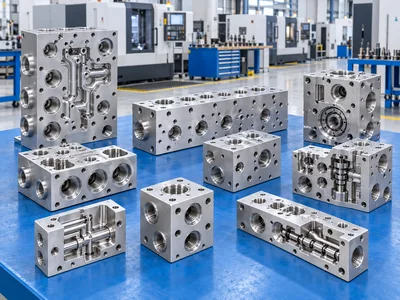
CNC Manifolds and Valve Bodies
Deep holes, intersecting channels, ports, sealing faces and internal-burr control.
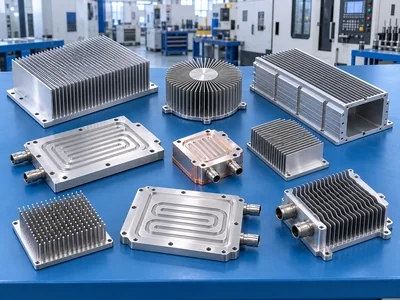
Heat Sinks & Thermal
Fins, grooves and flat thermal interfaces for electronics and cooling assemblies.
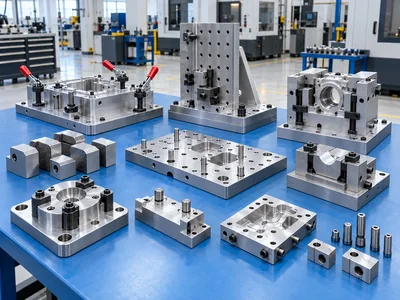
Fixtures and Tooling
Jigs, holding plates, fixture blocks and repeatable locating features.
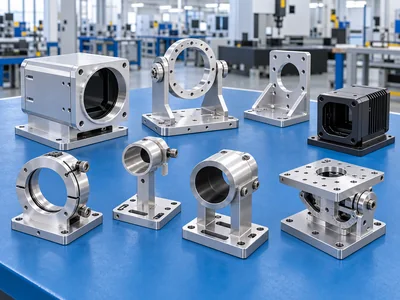
Sensor and Camera Mounts
Stable hole positions, angular relationships and controlled reference surfaces.
CNC Milling Processes Selected Around Your Geometry

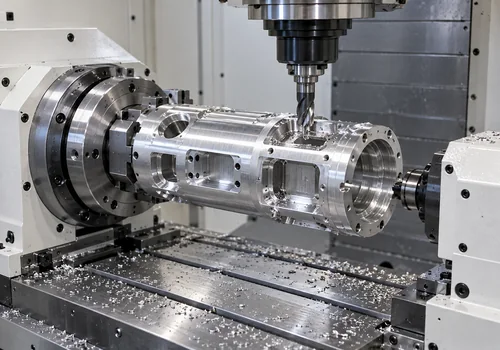
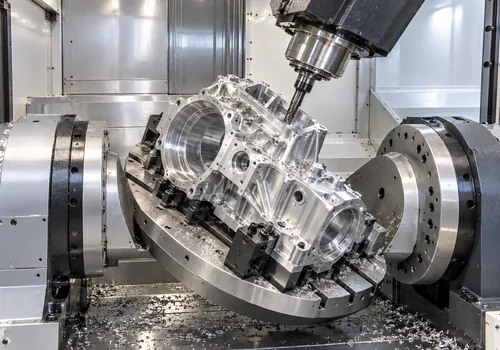
| Process | Suitable Features | Main Selection Consideration |
|---|---|---|
| 3-Axis CNC Milling | Plates, brackets, blocks, pockets and standard housings | Access from three primary directions |
| 4-Axis CNC Milling | Indexed side features and multi-face parts | Fewer re-clamping operations |
| Selected 5-Axis Milling | Angled surfaces and complex multi-side features | Better tool access and fewer setups |
| Drilling and Tapping | Mounting holes and threaded holes | Hole position, depth, thread fit and chip evacuation |
| Boring and Pocketing | Precision bores, cavities and internal features | Tool access, flatness and dimensional stability |
| Turn-Mill Support | Round components with milled flats, slots or cross holes | Combined operations where suitable |
The correct process is confirmed from the drawing, material, quantity, tolerance and inspection requirements. A machine list alone does not determine the best manufacturing route.
Materials for Precision CNC Milling Services
Material selection affects machinability, rigidity, weight, corrosion resistance, surface finish and total project cost. Confirm the exact grade and condition before production.
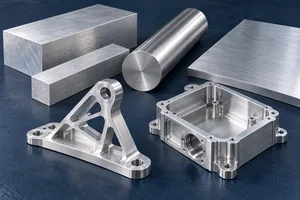
Aluminum
6061, 6063, 6082 and 7075 for lightweight housings, brackets, heat sinks, plates and structural parts.
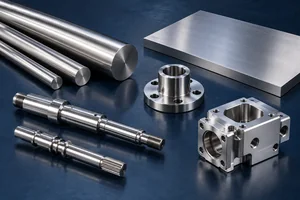
Stainless Steel
303, 304, 316 and 316L for corrosion-resistant components, connectors, fluid-control parts and equipment structures.
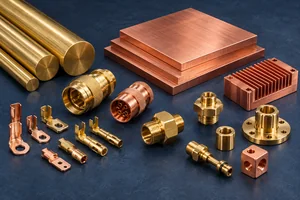
Brass and Copper
For electrical terminals, connector bodies, heat-transfer parts, inserts and precision fittings.
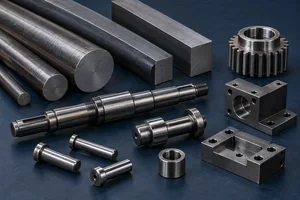
Carbon & Free-Machining Steel
For fixtures, machinery components, brackets and parts requiring strength or plated finishes.
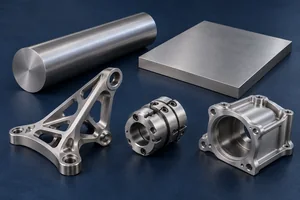
Titanium
For selected lightweight, high-strength and specialized applications when confirmed by the project requirement.
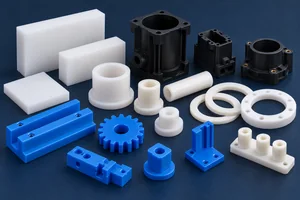
Engineering Plastics
POM, nylon, PTFE and other plastics for insulation, low friction, chemical resistance or weight reduction.
Note: Available materials and grades are confirmed during quotation. When the drawing does not specify a material, the final selection remains subject to engineering approval.
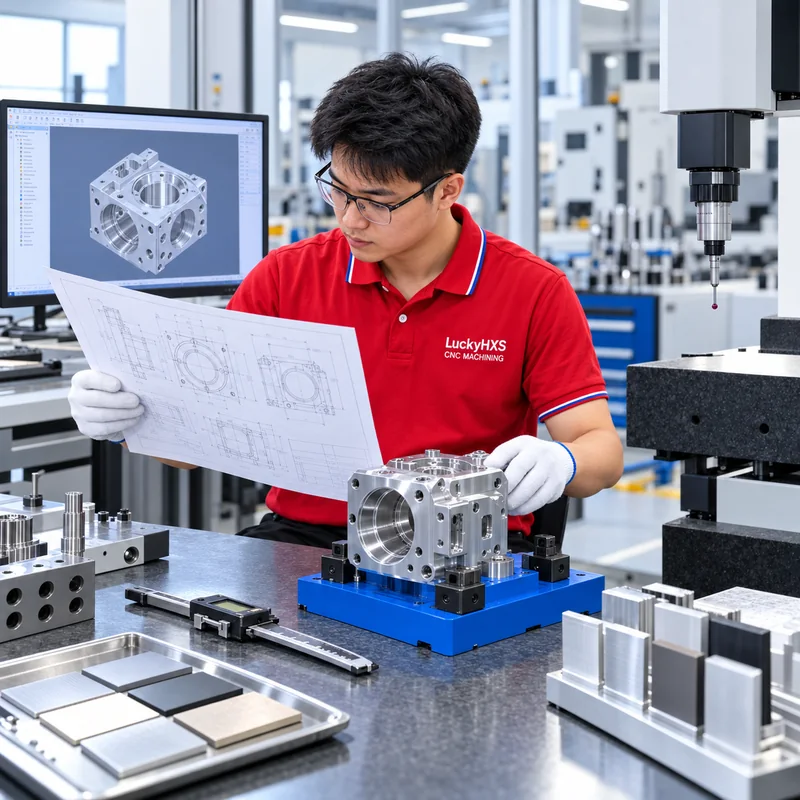
Precision CNC Milling Specifications to Confirm
- • Processes: 3-axis, 4-axis, selected 5-axis milling, drilling, tapping, boring, pocketing and turn-mill support
- • Tolerance: Standard reference up to ±0.01 mm for suitable features
- • Typical Features: Pockets, slots, holes, threads, flat faces, angled faces, ribs, bores and sealing surfaces
- • Materials: Aluminum, stainless steel, brass, copper, carbon steel, titanium and engineering plastics
- • Surface Finishes: As-machined, anodizing, sandblasting, polishing, passivation, black oxide, nickel plating and zinc plating where suitable
- • Drawing Formats: PDF, STEP, STP, IGES, IGS, DWG and DXF
- • Production Type: Prototypes, low-volume orders, pilot batches and repeat production
- • Inspection: Projector, 2D/3D inspection, CMM, gauges and dimensional inspection according to the project
- • MOQ: From 1 piece for many custom projects; final quantity depends on geometry and process
Caution: Actual capability depends on part size, material, feature accessibility, tolerance distribution, finishing and inspection method.
Design Review Before Material Is Cut
A part may be dimensionally correct and still fail assembly if the wrong features are prioritized. Precision CNC milling starts by connecting functional surfaces, datums, hole positions and tolerance direction.
Datum and Assembly Review
Mounting faces, hole patterns and mating features should use a clear functional reference.
Internal Corner Radii
Standard tool radii can reduce unnecessary machining time and improve tool access.
Deep Pockets and Thin Walls
Deep narrow cavities and thin sections require workholding and distortion review.
Hole and Thread Access
Hole depth, thread depth, tool clearance and chip evacuation affect process stability.
Flatness and Parallelism
Critical mounting and sealing faces should be identified before quotation.
Cosmetic Surfaces
Visible faces, clamp areas, tool marks and finish requirements should be separated from hidden features.
Common Precision Milling Risks and Practical Responses
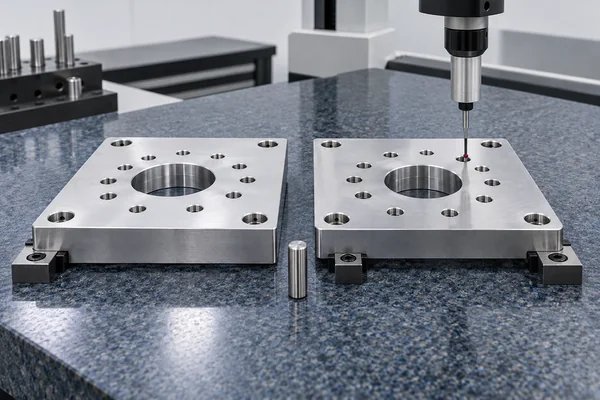
Hole Pattern Does Not Align
Risk: Mounting holes may be individually correct but misaligned as a pattern.
Response: Review functional datums, hole locations, fixture references and dedicated inspection methods.
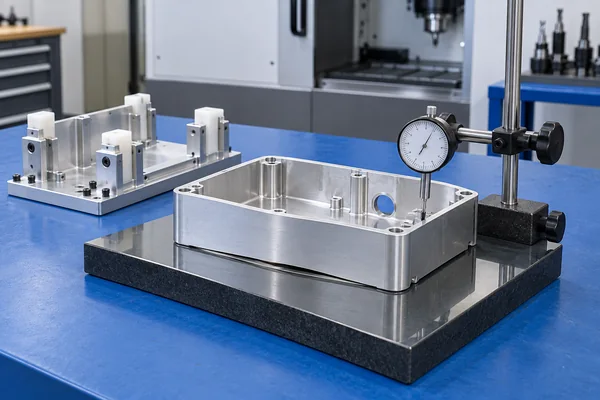
Thin Walls Warp After Unclamping
Risk: Clamping force, heat and residual stress may change the free-state geometry.
Response: Review workholding, machining sequence, wall thickness and post-unclamp inspection.
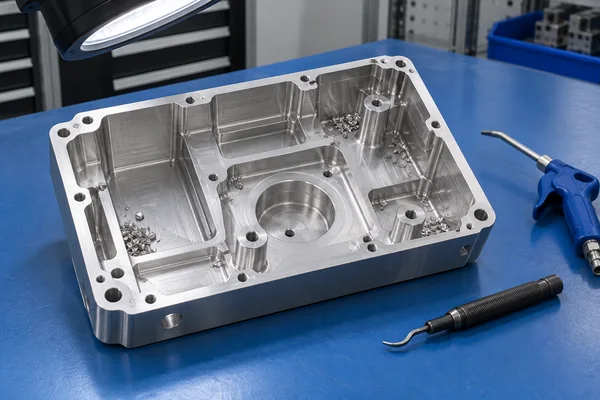
Deep Pockets Contain Burrs or Chips
Risk: Internal burrs and trapped chips can affect assembly, sealing and cleanliness.
Response: Define tool access, deburring, cleaning and inspection requirements before machining.
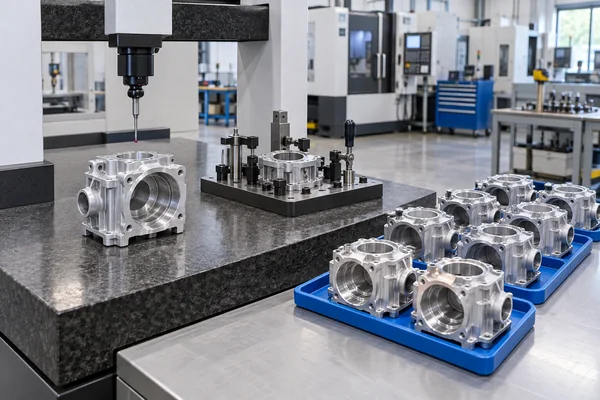
Prototype Does Not Transfer to Repeat Production
Risk: A sample process may not remain stable when quantity increases.
Response: Retain approved drawings, programs, fixture datums, material requirements and inspection points.
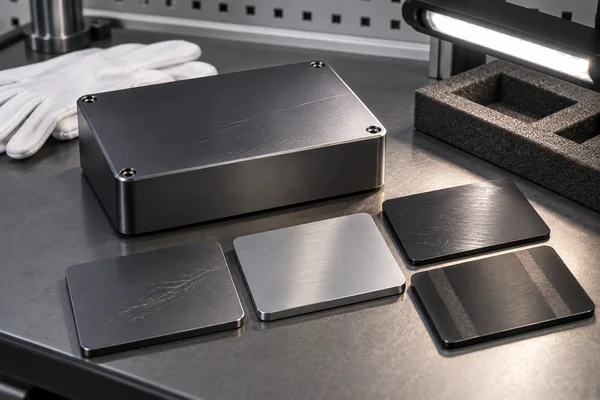
Cosmetic Surfaces Show Marks
Risk: Clamp marks, tool marks and scratches may remain visible after anodizing or plating.
Response: Identify appearance-critical areas, protection requirements and approved finish ranges.
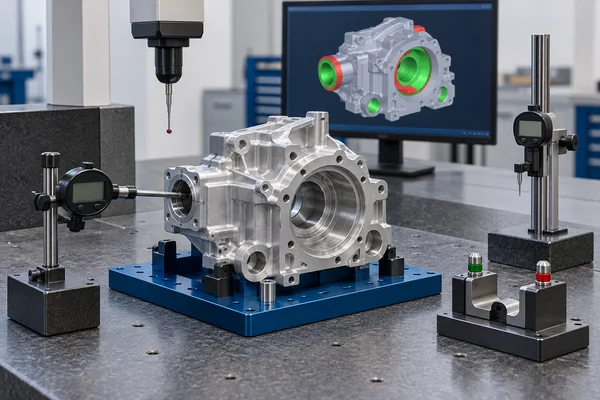
Tolerance Is Applied Too Broadly
Risk: Tight tolerances on non-critical surfaces increase cost without improving function.
Response: Separate critical-to-function dimensions from general dimensions during engineering review.
Inspection Based on Part Function
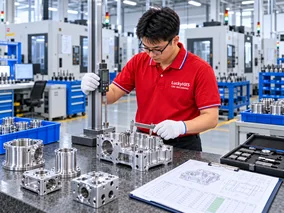
LuckyHXS selects inspection methods according to drawing requirements, feature accessibility and the function of the machined part.
-
1
Drawing Requirement Review Identify material, datums, critical dimensions, finish and assembly requirements.
-
2
Incoming Material Check Confirm the specified material and condition.
-
3
First Article Inspection Measure the first completed part before the production batch continues.
-
4
In-Process Inspection Monitor critical dimensions and tool-wear-sensitive features.
-
5
Final Dimensional Inspection Inspect hole positions, flatness, parallelism, perpendicularity, pockets and threads.
-
6
Packing Verification Confirm quantity, labels, surface protection and agreed documentation.
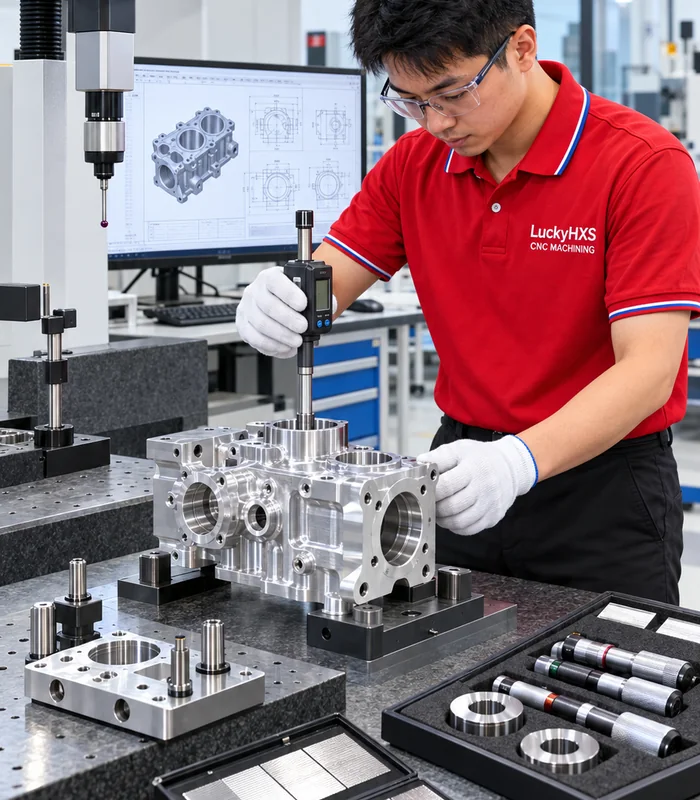
Visible Inspection Focus:
Surface Finishing for Precision CNC Milled Parts
Surface finishing should be selected around the part’s function, environment and appearance requirement. The final treatment can affect dimensions, color, surface texture and assembly fit.
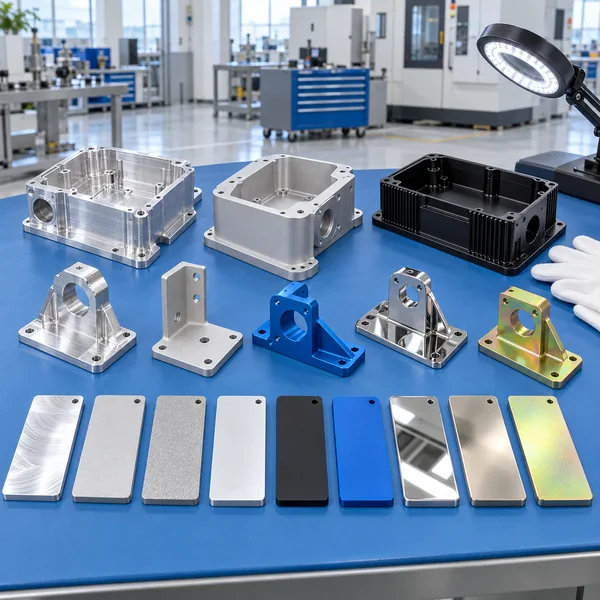
Surface Finishing Checklist
- • Identify cosmetic surfaces
- • Confirm coating thickness
- • Define masking areas
- • Confirm before-finish or after-finish dimensions
- • Review threads and bores after finishing
- • Approve color or appearance range
- • Protect finished surfaces during packaging
From Drawing Review to Delivered CNC Milled Parts
Send Drawings or CAD Files
Review Material and Critical Features
Confirm DFM and Machining Route
Prepare Quotation and Process Assumptions
Machine Prototype or First Article
Perform In-Process Inspection
Apply Surface Treatment
Complete Final Inspection
Verify Quantity and Packaging
Transfer Approved Requirements to Repeat Orders
The same drawing revision, inspection points and agreed process assumptions should remain visible as the project moves from sample approval to repeat manufacturing.
Applications for Precision CNC Milled Components
Industrial Automation
Positioning blocks, brackets, fixture plates and equipment housings.
Robotics & Machinery
Mounting brackets, structural parts, sensor mounts and actuator components.
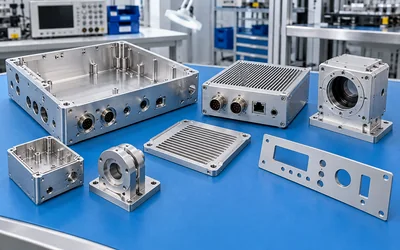
Electronics & Instrumentation
Controller housings, enclosures, heat sinks and precision mounting plates.
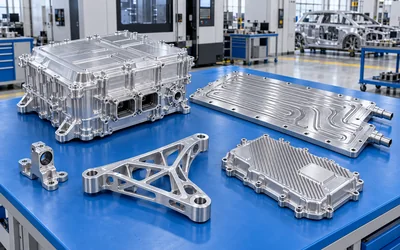
Automotive & EV
Control brackets, connector bodies, lightweight structural parts and fixtures.
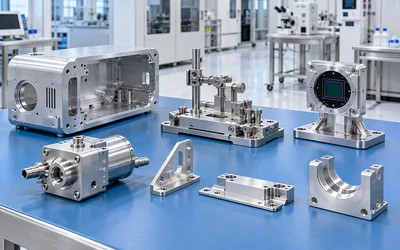
Medical Equipment
Instrument housings, sensor mounts and non-implantable equipment components, subject to project requirements.
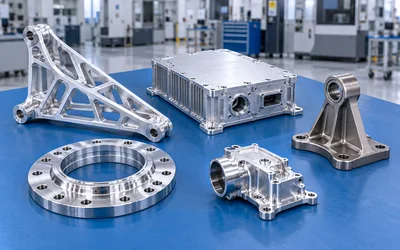
Aerospace & Defense
Lightweight structural parts, sensor enclosures and precision components subject to approved project specifications.
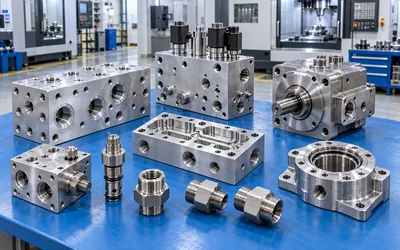
Fluid Control
Manifolds, valve bodies, pump blocks, adapters and flow-control components.
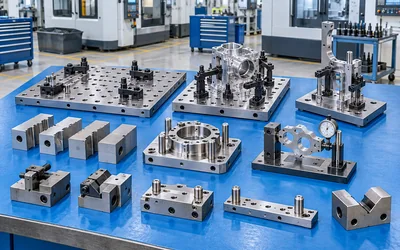
Industrial Tooling
Base plates, jigs, fixtures and locating components.
Published Precision CNC Milling Project Examples
Aerospace Sensor Enclosure
- Material: Aluminum 7075
- Process: 5-axis CNC milling
- Inspection: CMM and 100% visual inspection
- Engineering focus: Weight control, burr control and selected critical features
Published result: Selected critical features controlled to ±0.004 mm for the documented project scope.
EV Charging Control Bracket
- Material: Aluminum 6061
- Process: 4-axis CNC machining
- Inspection: Dedicated hole-pattern gauge
- Engineering focus: Mounting-hole alignment across repeat production.
Thin-Wall Equipment Housing
- Part type: Thin-wall machined enclosure
- Engineering focus: Flatness, wall stability, datum relationships, cosmetic surfaces and post-finish fit.
Manufacturing response: Controlled workholding, balanced material removal and free-state inspection.
A Precision CNC Milling Factory You Can Review
LuckyHXS CNC is the precision machining division of Shenzhen Hongxiangsheng Technology Co., Ltd. Our team supports drawing review, CNC milling, CNC turning, Swiss machining, turn-mill machining, inspection and export packaging for custom projects.
Precision CNC Milling from Prototype to Repeat Batch
A prototype proves the initial geometry. Repeat production also requires stable material, controlled fixtures, approved drawing revisions, repeatable inspection and clear packaging requirements.
Prototype
Confirm geometry, material, fit, finish and assembly concerns.
Pilot Batch
Review process stability, tool access, inspection points and production communication.
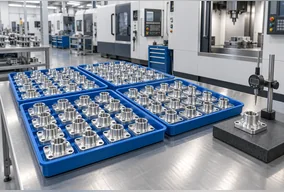
Repeat Production
Retain approved drawings, fixture datums, machining programs, material requirements and packaging instructions.
What Affects Precision CNC Milling Cost and Lead Time?
The cost of a precision CNC milled part depends on the complete manufacturing route, not only material price or machine time.
- ✓ Material grade and raw-stock size
- ✓ Number of setups and machining faces
- ✓ Pocket depth and tool-access difficulty
- ✓ Thin-wall and distortion-control requirements
- ✓ Hole, thread, bore and tolerance complexity
- ✓ Surface finish, anodizing and masking
- ✓ Quantity and repeat frequency
- ✓ Inspection records and packaging
- ✓ Drawing completeness and revision control
A complete drawing allows the quotation to reflect actual process assumptions instead of a generic unit-price estimate.
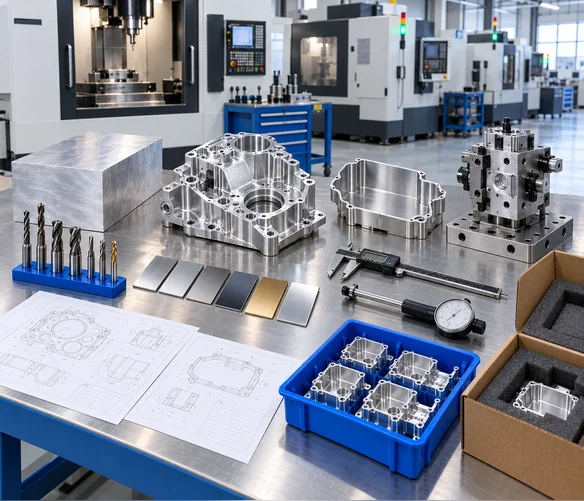
CNC Milling, Turning or Turn-Mill: Which Route Fits?
| Part Requirement | Recommended Route | Reason |
|---|---|---|
| Flat faces, pockets, slots and hole patterns | CNC Milling | Suitable for prismatic and multi-face parts |
| Cylindrical shafts, pins and sleeves | CNC Turning | Suitable for rotational geometry |
| Round parts with flats, cross holes or slots | Turn-Mill | Combines rotational and milling features |
| Small long parts with dense features | Swiss Machining | Suitable for small-diameter precision components |
The final process route is selected after reviewing the complete part geometry, material, quantity, tolerance and inspection requirements.
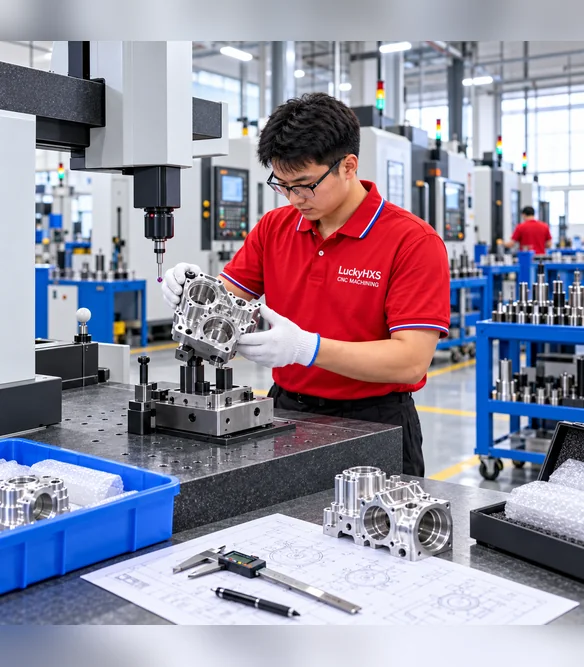
How to Choose a Precision CNC Milling Manufacturer
- 1 Can the supplier review the complete drawing instead of only the material?
- 2 Can the supplier machine thin walls, deep pockets and multi-face parts?
- 3 Can the supplier control functional datums and hole patterns?
- 4 Can the supplier inspect flatness, parallelism and perpendicularity?
- 5 Can the supplier manage burrs in deep pockets and cross holes?
- 6 Can the supplier review surface-finish and anodizing effects?
- 7 Can the supplier support prototype and repeat production?
- 8 Can the supplier provide inspection or material documents?
- 9 Can the supplier protect cosmetic surfaces during packaging?
- 10 Can the supplier retain approved drawing revisions?
- 11 Can the supplier support multiple materials and machining routes?
- 12 Can the supplier protect confidential CAD files and technical data?
A suitable manufacturer should be evaluated against the actual drawing, material, tolerance, finish, quantity and inspection requirements.
Explore Related LuckyHXS CNC Capabilities
Precision CNC Milling Services FAQ
What are precision CNC milling services used for?
What materials can LuckyHXS CNC mill?
Can you support 3-axis, 4-axis and 5-axis milling?
What tolerance can precision CNC milling achieve?
Can you manufacture prototypes and repeat batches?
How do you control thin-wall CNC milled parts?
Can you machine internal threads and deep pockets?
Can CNC milled parts receive anodizing or plating?
What files are needed for a quotation?
How should I reduce CNC milling cost?
What to Send for a Precision CNC Milling Quote
If some information is not available, send the current drawing and explain the part’s application. Our engineering team can identify missing information before quotation.
Ready to Discuss Your Precision CNC Milling Project?
Send your drawing, CAD file or sample to LuckyHXS. Our team will review the material, machining route, critical features, tolerance, finish, inspection scope and production quantity before preparing a quotation.
- Drawing-based precision CNC milling
- 3-axis, 4-axis and selected 5-axis machining
- Custom housings, brackets, plates, enclosures, manifolds and fixtures
- Prototype, low-volume and repeat production
- DFM review for datums, hole patterns, thin walls and deep pockets
- Inspection documentation and NDA support according to project requirements
admin1@lucky-hxs.com
+86 13342931453