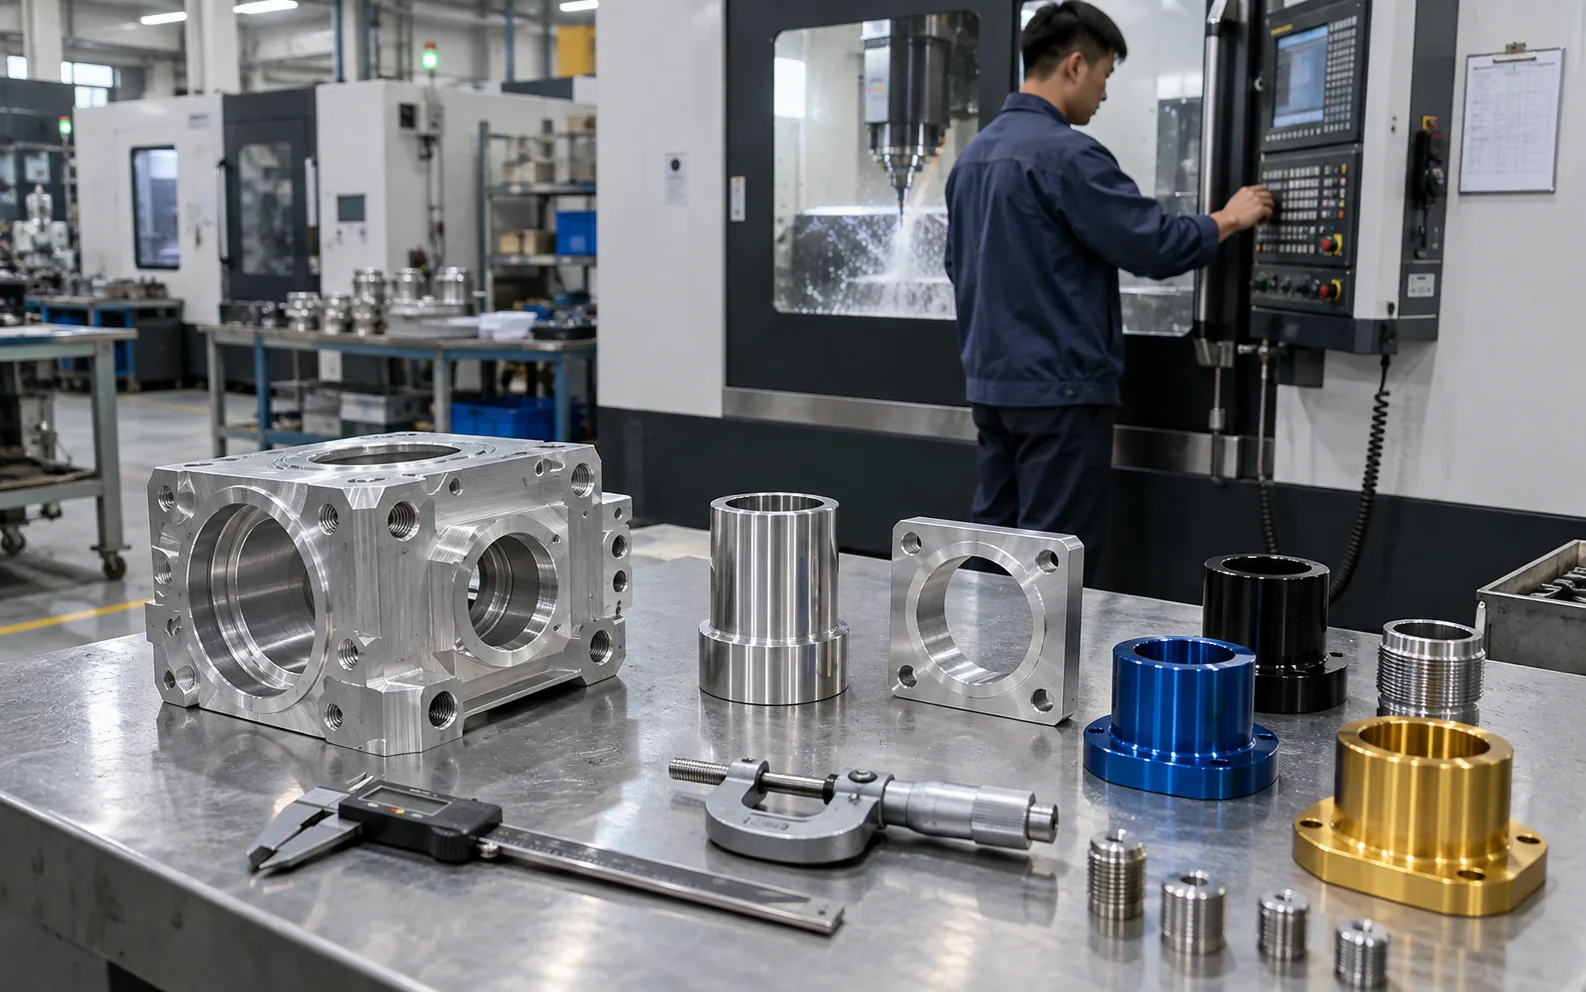
Anodizing improves corrosion resistance, wear performance, and appearance, but it also changes critical CNC dimensions. For anodized aluminum CNC parts, the coating grows into and out of the surface, affecting holes, threads, slots, bores, shafts, and press fits. Successful aluminum anodizing services start with tolerance planning, masking strategy, and machining offsets before finishing—not after inspection.
Dimensional Effects of Anodizing on CNC Aluminum Parts
Anodized aluminum CNC parts are machined aluminum components that receive an electrochemical oxide coating after milling, turning, or turn-mill machining. This coating improves durability, corrosion resistance, and appearance, but it changes dimensions. Critical features such as holes, threads, bearing fits, and sealing surfaces must be compensated before anodizing.
Definition and Dimensional Impact
Anodizing is not a paint layer sitting only on top of the part. It converts the aluminum surface into aluminum oxide through an electrochemical process. Because the oxide layer grows partly into the base metal and partly outward, dimensions change in measurable ways.
For aluminum CNC milling parts, the most affected features are flat locating faces, pockets, holes, slots, and counterbores. For aluminum CNC turned parts, the most affected features are outside diameters, inside diameters, grooves, bearing seats, and threaded sections. For precision aluminum turn-mill parts, both axial and radial features must be controlled together.
Based on our internal data and market analysis, here is the breakdown:
| Feature Type | Typical Anodizing Effect | Engineering Concern | Common Control Method |
|---|---|---|---|
| Outside diameter | Increases | Shaft may become too large | Machine undersize before anodizing |
| Inside diameter / hole | Decreases | Pin, screw, or dowel may not fit | Machine oversize before anodizing |
| External thread | Pitch diameter increases | Nut may bind | Oversize allowance or masking |
| Internal thread | Pitch diameter decreases | Screw may bind | Tap allowance, masking, or thread forming plan |
| Flat sealing face | Surface grows slightly | Seal compression may change | Masking or post-finish lapping |
| Sliding fit | Clearance decreases | Friction or seizure risk | Larger pre-anodize clearance |
Luckyhxs Pro Tip: I always ask customers to identify functional surfaces before quoting anodized aluminum CNC parts. Cosmetic faces, threaded holes, dowel holes, and bearing fits should not be treated the same way in the drawing or inspection plan.
How to Control CNC Tolerances Before and After Anodizing
Anodizing works by making the aluminum part the anode in an acid electrolyte, forming a controlled aluminum oxide layer. The coating thickness depends on anodizing type, alloy, current density, time, and sealing. Because the oxide grows on every exposed surface, holes shrink, shafts grow, and threads tighten.
Process Flow from Machining to Final Fit
The dimensional result depends on the full production route, not only the anodizing tank. A good process starts with the final functional requirement, then works backward to define pre-anodize machining dimensions.
Typical workflow:
- Review the drawing for tight tolerances, thread classes, dowel holes, bearing fits, and sealing surfaces.
- Confirm anodizing type, color, target thickness, and whether sealing is required.
- Calculate expected coating growth on exposed surfaces.
- Adjust CNC machining dimensions before finishing.
- Mask features that cannot tolerate coating buildup.
- Anodize using controlled bath parameters.
- Seal if required for corrosion resistance or dye stability.
- Inspect final dimensions after anodizing, not only before finishing.
A simplified rule often used for planning is that approximately half of the anodic coating grows outward and half penetrates into the aluminum substrate. For example, a 20 µm coating may create about 10 µm buildup per exposed surface. On a diameter, that can mean roughly 20 µm total dimensional change.
Based on our internal data and market analysis, here is the breakdown:
| Anodizing Type | Typical Thickness Range | Dimensional Sensitivity | Common Use |
|---|---|---|---|
| Type II sulfuric anodizing | 5–25 µm | Moderate | Decorative and corrosion-resistant parts |
| Type III hardcoat anodizing | 25–75 µm | High | Wear-resistant precision components |
| Clear anodizing | Usually thinner to moderate | Moderate | Functional and cosmetic parts |
| Black anodizing | Depends on Type II or III | Moderate to high | Optical, consumer, and industrial parts |
| Masked anodizing | Coating excluded locally | Controlled | Threads, bores, ground faces, electrical contact areas |
Luckyhxs Pro Tip: I do not recommend using the same tolerance strategy for Type II and hardcoat anodizing. Hardcoat can dramatically affect hole dimensions and thread tolerance, especially on small features.
Benefits of Anodizing for Precision CNC Aluminum Parts
The main benefits are corrosion resistance, improved wear performance, electrical insulation, better surface hardness, and stable appearance. When anodizing effects are planned correctly, CNC parts can maintain reliable holes, threads, and fits while gaining a durable oxide surface suitable for aerospace, robotics, medical, automotive, and electronics applications.
Functional Benefits Beyond Appearance
Anodizing is often selected for color, but its real value is functional. Aluminum oxide is harder and more chemically stable than bare aluminum, which makes anodized aluminum CNC parts more resistant to handling damage, oxidation, and sliding wear.
For precision aluminum turn-mill parts, anodizing can protect complex geometries without adding a separate coating material such as paint or plating. However, the benefit is strongest when the design accounts for coating growth.
Key benefits include:
- Corrosion resistance: Sealed anodizing improves protection in humid, industrial, and outdoor environments.
- Wear resistance: Hardcoat anodizing improves abrasion resistance on sliding or contact surfaces.
- Improved appearance: Clear, black, and dyed finishes provide consistent cosmetic quality.
- Electrical insulation: The oxide layer is non-conductive, useful in electronics housings and fixtures.
- Low added weight: Anodizing adds minimal mass compared with many coating systems.
- Better surface stability: The oxide layer is integral to the aluminum surface and does not peel like paint.
Based on our internal data and market analysis, here is the breakdown:
| Benefit | Best Anodizing Choice | Fit/Tolerance Consideration |
|---|---|---|
| Cosmetic finish | Type II dyed anodizing | Maintain uniform surface texture before anodizing |
| Wear resistance | Type III hardcoat | Increase clearance for moving fits |
| Corrosion protection | Sealed Type II or Type III | Avoid unsealed porous surfaces |
| Thread durability | Hardcoat with planned allowance | Control pitch diameter carefully |
| Electrical insulation | Type II or Type III | Mask grounding points if needed |
Luckyhxs Pro Tip: I prefer to define anodizing as an engineering requirement, not just a finish note. If the part has sliding fits, dowel holes, or threaded holes, the anodizing callout should include thickness and masking instructions.
How to Maintain Anodized CNC Parts for Reliable Fits and Threads
Maintain anodized aluminum CNC parts by cleaning with mild detergents, avoiding abrasive pads, protecting threaded and fitted areas from impact, and preventing contact with strong acids or alkalis. For precision parts, maintenance also includes checking wear surfaces, lubricating sliding fits, and avoiding thread damage during repeated assembly.
Care Methods for Long-Term Dimensional Reliability
Anodized surfaces are durable, but they are not indestructible. Hard abrasion, alkaline cleaners, aggressive chemicals, and improper assembly tools can damage the oxide layer. Once the layer is scratched through, the exposed aluminum may corrode or wear faster.
For threaded features, the biggest maintenance issue is galling or cross-threading. If anodizing has reduced clearance, repeated assembly can damage both the coating and the mating fastener. Lubrication and correct screw engagement are important.
Recommended maintenance practices:
- Clean with pH-neutral detergent and soft cloths.
- Avoid steel brushes, abrasive pads, or aggressive polishing compounds.
- Do not use strong alkaline cleaners unless approved for anodized aluminum.
- Use compatible fasteners to reduce galvanic corrosion.
- Apply suitable lubricant on sliding fits or frequently assembled threads.
- Inspect high-wear areas for coating loss.
- Protect precision bores and dowel holes during storage and transport.
- Avoid forcing screws into tight anodized internal threads.
Based on our internal data and market analysis, here is the breakdown:
| Maintenance Issue | Cause | Prevention |
|---|---|---|
| Thread binding | Reduced thread clearance after anodizing | Use correct thread tolerance and lubrication |
| Surface staining | Chemical attack or poor cleaning | Use mild cleaners and rinse thoroughly |
| Bore wear | Repeated pin insertion | Specify hardcoat or use bushings |
| Color fading | UV exposure or low dye stability | Use suitable sealing and color specification |
| Galvanic corrosion | Contact with dissimilar metals | Use compatible fasteners or isolation washers |
Luckyhxs Pro Tip: I always tell customers not to “fix” a tight anodized hole or thread with aggressive scraping unless engineering approves it. Removing anodizing locally can change corrosion resistance and fit consistency.
Anodized Aluminum CNC Machining Cost & Pricing Factors
The price depends on material, machining complexity, tolerance class, anodizing type, coating thickness, color, masking, inspection level, and order quantity. Hardcoat anodizing, tight thread tolerance, precision holes, and complex masking increase cost because they require more process control, handling, and post-anodize inspection.
Pricing Drivers for Machining and Anodizing
The cost of anodized aluminum CNC parts includes more than the anodizing bath. Tight-tolerance CNC machining, surface preparation, racking, masking, color control, sealing, packaging, and inspection all contribute to the final price.
Small parts may be inexpensive to anodize individually, but setup, minimum lot charges, and masking labor can dominate the cost. Large precision parts may cost more due to tank capacity, current control, handling risk, and inspection time.
Based on our internal data and market analysis, here is the breakdown:
| Cost Factor | Cost Impact | Why It Matters |
|---|---|---|
| Tight CNC tolerance | High | Requires slower machining and more inspection |
| Hardcoat anodizing | Medium to high | Thicker coating needs tighter process control |
| Black or dyed finish | Medium | Color consistency and sealing add control steps |
| Masked threads/bores | High | Manual masking increases labor |
| Small batch quantity | High per part | Setup and minimum charges spread over fewer units |
| Complex turn-mill geometry | High | More features require dimensional compensation |
| Final inspection report | Medium | Adds measurement and documentation time |
General pricing guidance:
- Simple machined aluminum parts with clear Type II anodizing are usually the most economical.
- Black anodizing typically costs more than clear anodizing due to dye control.
- Hardcoat anodizing costs more because of thickness, process time, and dimensional control.
- Masking precision threads, bearing bores, and electrical contact surfaces can significantly increase cost.
- High-volume production reduces per-part finishing and setup costs.
Luckyhxs Pro Tip: When I quote aluminum anodizing services, I prefer receiving both the CAD model and the 2D drawing. The CAD shows geometry, but the drawing tells us which dimensions must survive anodizing.
Key Features & Comparison
The key features of anodized aluminum CNC parts include controlled coating thickness, improved hardness, corrosion protection, color options, electrical insulation, and predictable dimensional compensation. The best choice depends on whether the priority is cosmetic quality, wear resistance, tight holes, thread tolerance, or precision mechanical fit.
Comparison of Common Anodizing Choices
Based on our internal data and market analysis, here is the breakdown:
| Feature | Type II Anodizing | Type III Hardcoat Anodizing | Masked Anodizing | No Anodizing |
|---|---|---|---|---|
| Typical purpose | Cosmetic and corrosion protection | Wear resistance and durability | Selective protection | Lowest cost, raw aluminum |
| Coating thickness | Lower to moderate | Higher | Controlled by exposed areas | None |
| Effect on holes | Moderate shrinkage | Significant shrinkage | Avoided in masked holes | No coating change |
| Effect on threads | Moderate tightening | High tightening risk | Threads can remain functional | No coating protection |
| Wear resistance | Good | Excellent | Depends on exposed areas | Low |
| Corrosion resistance | Good when sealed | Very good when sealed | Good on coated areas | Limited |
| Cost | Moderate | Higher | Higher due to labor | Lowest |
| Best for | Housings, brackets, panels | Sliding parts, tooling, wear surfaces | Precision assemblies | Prototypes or non-exposed parts |
Anodizing selection should match the functional requirement. For example, Type II is often sufficient for aluminum CNC milling parts used as brackets, housings, and panels. Hardcoat anodizing is better for sliding surfaces, high-wear components, and precision aluminum turn-mill parts exposed to repeated mechanical contact.
For holes and threads, the key question is whether the anodized layer is needed inside the feature. If corrosion protection is required inside a hole, the machining allowance must account for reduced diameter. If the hole is a precision dowel fit, masking or post-process sizing may be required.
Decision checklist:
- Is the feature cosmetic, functional, or both?
- Does the surface need wear resistance?
- Is the hole a clearance hole, dowel hole, threaded hole, or bearing bore?
- Should the thread be anodized, masked, or post-processed?
- What final tolerance must be inspected after anodizing?
Luckyhxs Pro Tip: I treat anodizing thickness as part of the tolerance stack. If a bore has only 20 µm of clearance and the anodizing process can change the diameter by a similar amount, the design needs adjustment before production.
Cost & Buying Factors
Buying anodized aluminum CNC parts requires evaluating machining accuracy, anodizing thickness, alloy choice, finish color, masking requirements, inspection standards, and supplier process control. The lowest unit price is not always the lowest total cost if parts fail after anodizing due to tight holes, poor threads, or inconsistent fits.
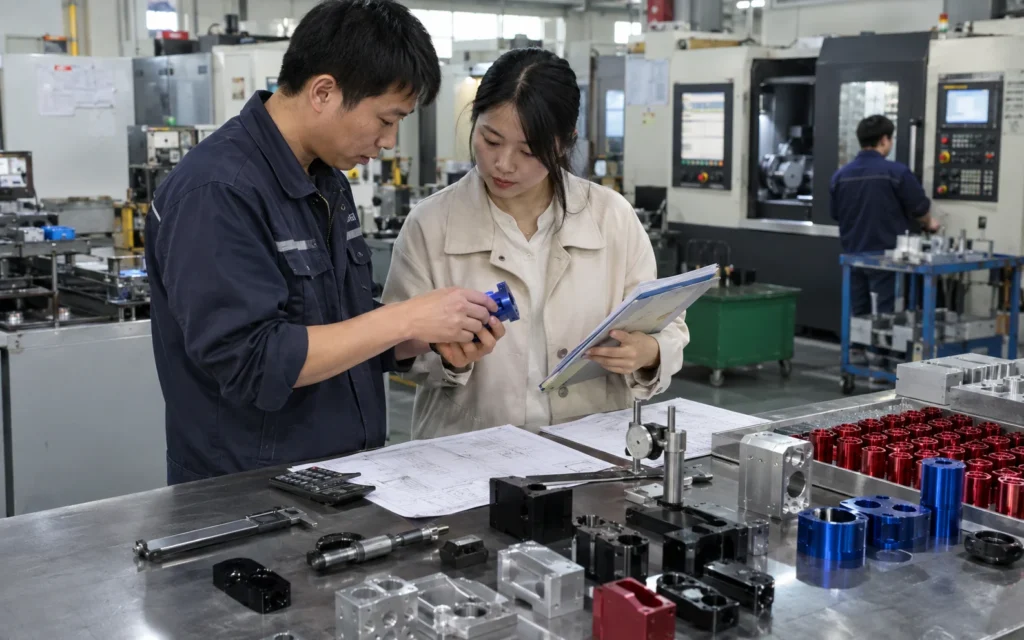
How to Specify and Purchase Correctly
A reliable purchase order should clearly define both machining and finishing requirements. Vague notes such as “black anodize” are often not enough for precision parts. For critical components, include anodizing type, thickness range, sealing requirement, color, masking areas, and final inspection criteria.
Important buying factors:
- Aluminum alloy: 6061, 6082, and 7075 respond differently in color, hardness, and dimensional stability.
- Anodizing type: Type II and Type III have very different thickness and tolerance effects.
- Surface finish before anodizing: Tool marks and polishing differences remain visible after anodizing.
- Masking requirement: Threads, bores, contact pads, and sealing faces may need selective protection.
- Tolerance after finish: State whether dimensions apply before or after anodizing.
- Inspection method: Define gauges, CMM inspection, thread gauges, pin gauges, or coating thickness measurement.
- Batch consistency: Color and thickness should be controlled across production lots.
Based on our internal data and market analysis, here is the breakdown:
| Buying Requirement | What to Specify | Risk if Ignored |
|---|---|---|
| Coating thickness | Type II or III with thickness range | Unexpected hole or thread changes |
| Thread tolerance | Final thread class after anodizing | Screw binding or loose assembly |
| Hole dimensions | Final diameter after finish | Dowel or pin fit failure |
| Masking | Drawing-marked no-anodize zones | Coating on functional surfaces |
| Color | Clear, black, or custom color standard | Lot-to-lot mismatch |
| Inspection | Final inspection after anodizing | Parts pass machining but fail assembly |
| Packaging | Scratch protection and separation | Cosmetic damage in transport |
A strong supplier should understand both CNC machining and finishing. Luckyhxs supports aluminum CNC milling parts, aluminum CNC turned parts, and precision aluminum turn-mill parts with anodizing planning, dimensional compensation, and practical DFM feedback.
Luckyhxs Pro Tip: I recommend marking all “critical after anodize” dimensions directly on the drawing. This prevents confusion between machine-shop inspection and final finished-part inspection.
Conclusion
Anodizing is an excellent finish for aluminum CNC parts, but it must be engineered into the tolerance plan. Holes shrink, outside dimensions grow, threads tighten, and precision fits can change. With correct machining offsets, masking, inspection, and supplier communication, anodized parts can be both durable and dimensionally reliable.
Final Engineering Takeaway
The most common anodizing problems are not caused by the coating itself. They happen because the coating was treated as an afterthought. If anodizing thickness, thread tolerance, and hole dimensions are considered during design and CNC programming, the final parts are far more predictable.
For successful anodized aluminum CNC parts:
- Define anodizing type and thickness early.
- Identify all critical holes, threads, and fits.
- Decide which surfaces require masking.
- Adjust machining dimensions for expected coating growth.
- Inspect final dimensions after anodizing.
- Work with a supplier that understands both machining and finishing.
Luckyhxs provides aluminum anodizing services for aluminum CNC milling parts, aluminum CNC turned parts, and precision aluminum turn-mill parts, helping customers control dimensions from machining through final surface treatment.
Luckyhxs Pro Tip: If your assembly depends on tight fits, send us the mating part information too. I can often help adjust clearances before machining so the anodized parts assemble correctly the first time.