
Precision CNC turning services convert a controlled drawing, 3D model, or approved sample into finished rotational components such as shafts, pins, sleeves, bushings, spacers, threaded connectors, fittings, and other made-to-order parts. The service may include process selection, material review, CNC turning, secondary features, finishing, inspection, documentation, packaging, and support for repeat orders.
LuckyHXS supplies drawing- and sample-based metal and engineering-plastic components. Its manufacturing scope includes conventional CNC turning, Swiss-type machining, turn-mill machining, milling, deburring, finishing coordination, and project-specific inspection. The exact process, tolerance capability, material availability, documentation, order quantity, and schedule must be confirmed from the actual RFQ. Review the commercial scope on the CNC turning service page, then close the technical and acceptance decisions below before releasing a precision turning project.
1. What Is Included in a Precision CNC Turning Service?
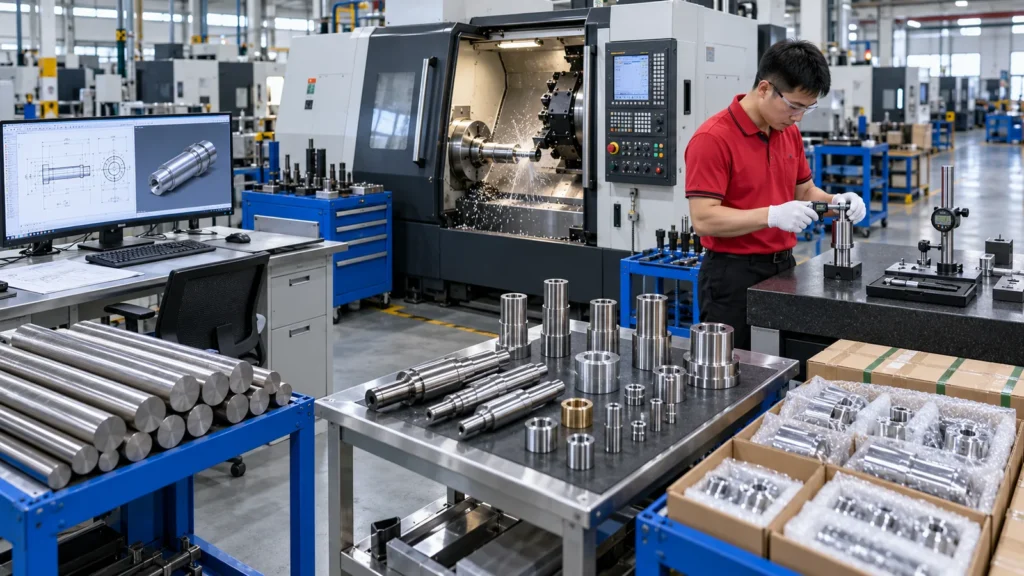
A precision CNC turning service should cover the complete agreed manufacturing scope, not only the time spent cutting the part on a lathe. The supplier receives the buyer’s requirements, selects a suitable process route, machines the part, completes agreed secondary operations, verifies the required characteristics, and releases the finished components in the specified condition.
A project may include:
- Review of the 2D drawing, 3D model, material, quantity, finish, and application requirements
- Selection of conventional CNC turning, Swiss-type machining, turn-mill machining, or a combined route
- Tooling, workholding, bar-stock, chucking, cutoff, and setup planning
- Facing, OD turning, boring, drilling, threading, grooving, tapering, chamfering, and parting
- Flats, cross holes, slots, side threads, or other off-axis features where required
- Deburring, cleaning, polishing, plating, anodizing, passivation, black oxide, or another specified finish
- First-part, in-process, and final verification according to the agreed inspection plan
- Inspection records, material documents, packaging, and shipment requirements when included in the order
The quotation should state which of these activities are included and which are excluded or supplied by an outside processor. A low turning price is not a complete comparison if the buyer must separately arrange deburring, finishing, inspection, or protective packaging.
2. Which Part Geometries Are Best Suited to Precision CNC Turning?
Precision CNC turning is usually the best starting process when the component is primarily rotational and most critical features are organized around a common axis. Typical examples include shafts, pins, sleeves, bushings, spacers, collars, threaded bodies, connectors, fittings, valve components, and cylindrical housings.
Turning is especially relevant when the drawing contains several of these features:
- Related outside and inside diameters
- Axial faces and shoulders
- Bores, counterbores, and centerline holes
- Internal or external threads
- Circumferential grooves, undercuts, and O-ring features
- Tapers, radii, chamfers, and sealing diameters
- Bearing, locating, press-fit, sliding-fit, or rotating surfaces
The part name does not determine the process. A round-looking component may still require substantial milling, grinding, EDM, or another secondary method. Conversely, a rotational part with a few flats or cross holes may remain a strong turning candidate if those features can be integrated efficiently.
For a process-level explanation, review What Is CNC Turning?. For feature-specific questions about finished components, use the precision CNC turned parts FAQ.
3. Should the Supplier Use Conventional Turning, Swiss Machining, or Turn-Mill Machining?
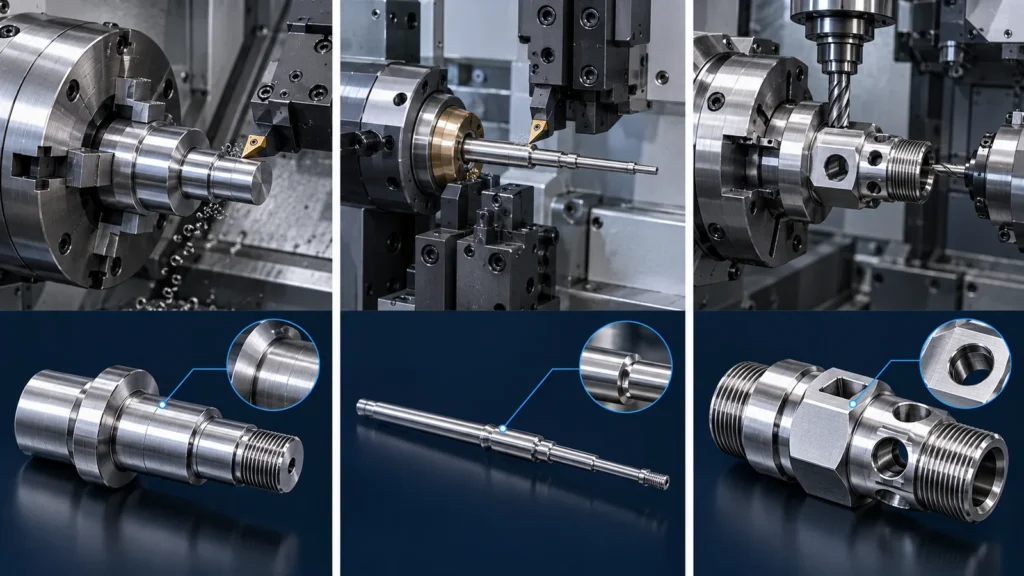
The supplier should select the route from the part’s geometry, material, length-to-diameter ratio, feature relationships, quantity, inspection needs, and finished condition. No process is automatically more precise or more economical for every component.
Conventional CNC turning is a practical route for many short, rigid, rotational components such as shafts, bushings, spacers, sleeves, fittings, and threaded bodies. It can establish several related diameters, bores, faces, and grooves around one spindle axis.
Swiss-type machining becomes relevant for selected small-diameter, slender, bar-fed, or feature-dense components. Supporting the stock near the cutting zone can reduce unsupported length, but actual suitability still depends on bar condition, machine configuration, tooling, geometry, and production requirements. The Swiss CNC machining service page explains the process fit in more detail.
Turn-mill machining is useful when a rotational part also contains flats, cross holes, slots, keyways, radial threads, or other off-axis features whose relationship to the turned geometry matters. Combining operations may reduce transfers, but a separate turning and milling route can still be more suitable for some parts. Review CNC turning and milling services when the drawing contains both feature families.
Ask the supplier to identify the proposed machine type, number of setups, workholding approach, datum strategy, cutoff plan, secondary operations, and inspection method. That explanation is more useful than a machine name or equipment list alone.
4. What Part Sizes Can a Precision CNC Turning Service Handle?
There is no universal minimum or maximum part size for precision CNC turning. Capacity depends on the supplier’s specific chuck, collet, spindle bore, bar feeder, guide bushing, tailstock, sub-spindle, tooling clearance, and inspection equipment. A quoted size range also needs context: a machine may physically accept a diameter or length that is not practical for the drawing’s material, wall thickness, tolerance, or production quantity.
For a meaningful capability check, send or confirm:
- Finished maximum and minimum outside diameters
- Bore diameter, bore depth, and length-to-diameter ratio
- Overall length and unsupported slender sections
- Raw-stock diameter, stock form, and available machining allowance
- Thin walls, deep grooves, long threads, and back-side features
- Required runout, straightness, roundness, and surface texture
- Quantity, cutoff method, and whether the part will be bar-fed or individually chucked
- Measurement access and any special gauges or inspection records
Short rigid parts, long shafts, thin sleeves, and miniature pins create different workholding and measurement risks even when their nominal diameters fit the same machine. Ask the supplier to confirm the proposed holding method, support strategy, number of setups, and inspection method for the actual drawing rather than accepting a maximum-diameter statement as proof of capability.
5. What Files and Information Should Be Sent for a CNC Turning Quote?
A useful RFQ should define the finished part, not just its nominal shape. Send a controlled 2D drawing and a matching 3D model where available, then add the material, quantity, finishing, inspection, packaging, and delivery information needed to plan the full route.
Include:
- Part number, drawing revision, and issue date
- Searchable PDF drawing with dimensions, tolerances, datums, GD&T, threads, surface texture, and edge notes
- STEP or STP solid model; native CAD only when compatibility is confirmed
- Exact material grade, standard, condition, hardness, and stock-form requirements
- Prototype quantity, initial order quantity, repeat quantity, and forecast where available
- Critical OD, ID, length, fit, runout, thread, groove, and sealing requirements
- Off-axis features and their relationship to the turned axis or functional datums
- Heat treatment, coating, plating, masking, polishing, cleaning, and final-condition requirements
- Required inspection scope, sampling rule, report format, and material or process documents
- Packaging, identification, destination, delivery basis, and required receipt date
State which file governs if the 2D drawing and 3D model conflict. Remove obsolete revisions before sending the package. If only a physical sample is available, identify which wear, damage, deformation, coating buildup, or previous repair must not be copied, and agree who will approve the reconstructed specification.
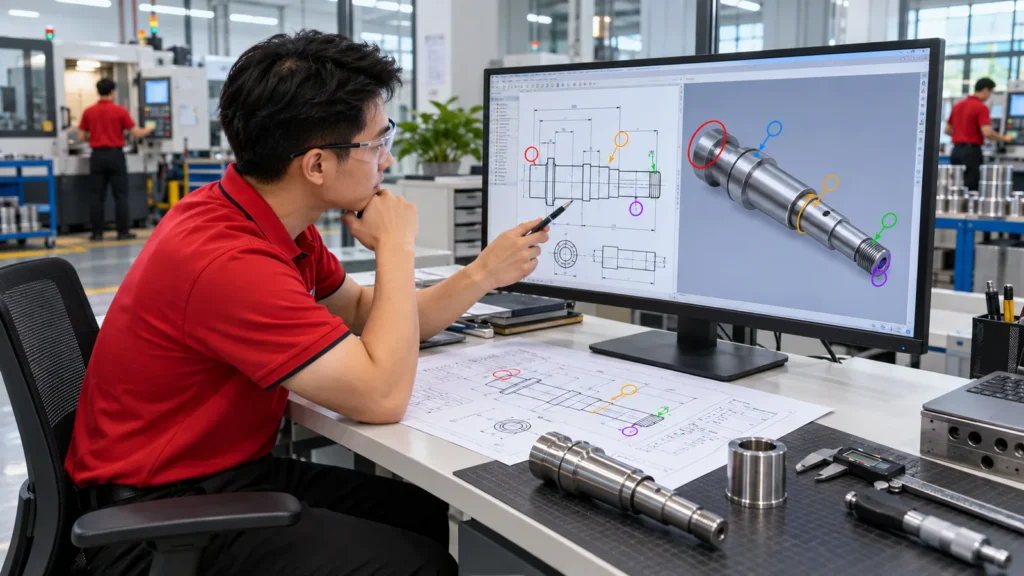
6. What Should Happen During a DFM Review for a Turned Part?
A turning DFM review should convert the buyer’s design intent into a practical manufacturing and inspection plan without changing functional requirements without approval. It should identify unclear, conflicting, difficult, or cost-sensitive requirements before material and tooling are committed.
The review should examine:
- Whether the part is mainly rotational and which process route fits it
- Raw-stock size, stock form, bar condition, and material availability
- Workholding surfaces, chucking or collet pressure, and cutoff access
- Tool access to bores, grooves, threads, shoulders, and back-side features
- Long slender sections, thin walls, deep bores, interrupted cuts, and deformation risks
- Datum selection and relationships between diameters, bores, faces, and off-axis features
- Whether finishing or heat treatment changes dimensions or distorts the part
- Burr, chip-removal, cleanliness, and protected-edge requirements
- Measurement access, inspection method, and report requirements
- Opportunities to relax nonfunctional tolerances or simplify features with buyer approval
A DFM response should distinguish between a requirement that is feasible as drawn, one that needs clarification, and one that needs a controlled design change. It should not silently widen a tolerance, substitute a material, change a finish, or remove an inspection requirement.
7. Which Materials Can Be Used, and Why Does Stock Condition Matter?
Precision turning can be applied to many metals and engineering plastics, but the exact grade and stock condition must be confirmed for the part and process. LuckyHXS supports project-specific review of aluminum, stainless steel, brass, copper, free-machining steel, carbon steel, POM, PTFE, and other requested materials; availability and supporting documents should be confirmed during quotation.
Material affects tool wear, cutting heat, chip control, burr formation, thread quality, surface finish, distortion, corrosion behavior, conductivity, weight, and compatibility with finishing. A family name such as “stainless steel,” “brass,” or “plastic” is not a complete purchasing specification.
Specify:
- Exact alloy or polymer grade and governing standard
- Temper, hardness, heat-treatment condition, or resin grade
- Bar, tube, billet, casting, forging, or customer-supplied blank
- Diameter, straightness, roundness, surface, and lot requirements where they affect the process
- Material certification, traceability, restricted-substance, or compliance documents required
- Whether alternatives are prohibited, permitted, or subject to written engineering approval
Stock condition matters because a correct material grade can still create machining or inspection problems if the bar is bent, inconsistent in diameter, heavily scaled, internally stressed, or unsuitable for the selected workholding route. Material approval and process approval should therefore be treated as related but separate decisions.
8. What Tolerances Can Precision CNC Turning Services Hold?
Tolerance capability must be confirmed feature by feature from the actual drawing. The word “precision” does not establish one universal tolerance, and a supplier’s general capability statement does not prove that every diameter, bore, length, thread, wall, or runout requirement is achievable under every condition.
Capability depends on:
- Material and stock condition
- Feature size, depth, length, wall thickness, and accessibility
- Workholding force and unsupported length
- Tooling, insert condition, machine stability, and thermal behavior
- Number of setups and relationship between separately machined features
- Required surface texture and finishing sequence
- Production quantity and tool-wear control
- Measurement method, fixture, temperature, sampling, and report requirement
Define the functional characteristics first. A bearing seat, sealing diameter, press fit, locating shoulder, mating bore, effective thread, or rotating surface may need close control, while a clearance feature may not. For each critical feature, state the datum, tolerance, final condition, and acceptance method.
Do not confuse machine positioning resolution with finished-part capability. Ask the supplier to confirm how the requirement will be machined, measured, and maintained across the order. Tightening every dimension can add setups, tool changes, slower cycles, secondary processing, inspection time, and scrap risk; the article on how tight tolerances affect CNC machining cost provides additional context.
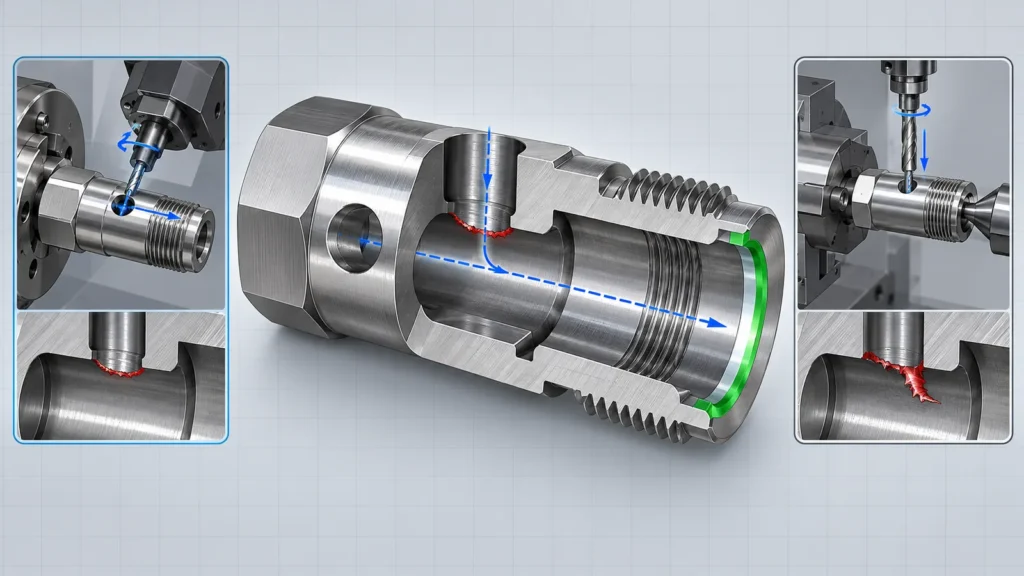
9. Can Precision CNC Turning Include Flats, Cross Holes, Slots, and Side Threads?
Yes. Off-axis features can be produced with live tooling, turn-mill machining, or separate milling and drilling operations, provided the complete route is included in the quotation. Common additions include wrench flats, milled faces, cross holes, radial holes, slots, keyways, side threads, bolt circles, engraving, and orientation-sensitive features.
The buyer should define more than feature size. Specify:
- Axial and angular position relative to the functional datum
- Relationship to a bore, thread, shoulder, flat, or sealing surface
- Internal burr and chip-removal requirements at intersecting passages
- Edge break, chamfer, or protected-edge requirements
- Orientation and marking requirements
- Final inspection method and record, if required
Ask which features will be completed in the main turning setup and which require reclamping or transfer. A second setup can be completely acceptable, but the supplier must explain how the datum relationship will be restored and inspected. If a cross hole intersects a bore or thread, include the hidden internal edge in the deburring and cleanliness requirements. The deburring services page provides a useful starting point for defining feature-specific edge conditions.
10. How Do Finishing and Heat Treatment Affect a CNC Turning Quote?
Finishing and heat treatment affect dimensions, sequence, masking, inspection, appearance, corrosion behavior, and schedule, so they must be defined before the turning process is finalized. The supplier needs to know the required final condition, not only the as-machined geometry.
Clarify:
- Exact finish or heat-treatment process and governing specification
- Surfaces to coat, plate, polish, grind, passivate, blacken, anodize, or protect
- Required thickness, hardness, texture, color, or cosmetic standard where applicable
- Threads, bores, fits, contacts, sealing faces, and datum surfaces that need masking
- Dimensions and gauges that apply after processing
- Machining or grinding allowance before the final process
- Reinspection and documentation required after outside processing
Plating adds material to exposed surfaces and can change outside diameters, bores, threads, and press fits. Polishing and grinding remove material. Heat treatment may change hardness and geometry. Anodizing and other conversion or coating processes can affect fit and appearance. The drawing should identify whether each critical requirement applies before or after finishing.
Review the surface finishing service page and the explanation of whether drawing dimensions apply before or after finishing before releasing the RFQ.
11. How Should Precision CNC Turned Parts Be Inspected?
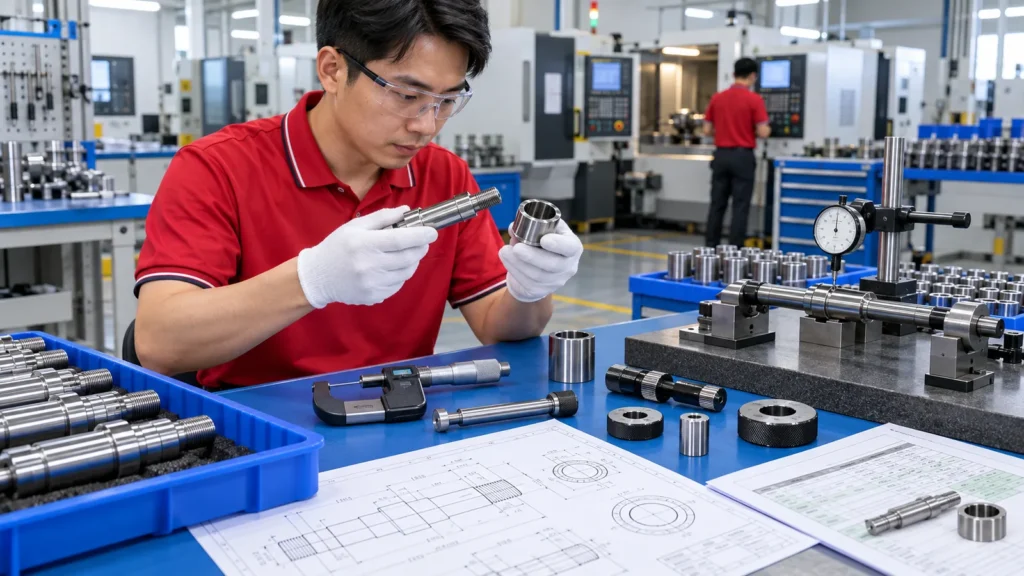
Inspection should be planned from the drawing’s functional features, not from a generic list of measuring equipment. The agreed plan should identify what is checked, at which production stage, against which revision, with which method, at what frequency, and in what report format.
Depending on the part, inspection may cover:
- OD, ID, overall length, shoulder position, step length, and wall thickness
- Bore size, depth, fit, taper, and relationship to outside diameters
- Circular or total runout and other rotational relationships to a datum axis
- Internal and external thread size, usable length, entry, exit, and burr condition
- Groove width, depth, diameter, radius, and position
- Cross-hole position, angular orientation, and intersection condition
- Surface texture, cosmetic surfaces, sharp edges, cleanliness, and identification
- Final dimensions after heat treatment, coating, plating, polishing, or grinding
- Packaging condition and protection of threads, sealing faces, and cosmetic areas
Hand tools can be suitable for many direct dimensions. Bore gauges, pin gauges, thread gauges, indicators, optical methods, height gauges, or CMM inspection may be appropriate for other characteristics. The method should match the feature and its function; a CMM is not automatically required for every dimension.
Before ordering, state whether you need first-part results, a first-article report, selected critical-characteristic data, a full dimensional report, material documents, finish records, process certificates, or photographs. Required documents should be priced and agreed before production. See CNC machining quality inspection for a feature-based inspection framework.
12. How Does a Prototype Move Into Repeat CNC Turning Production?
An approved prototype should become a controlled production reference, not an informal visual sample. Before repeat production, connect the approved part to the released drawing revision, material requirement, process route, finishing specification, inspection plan, and packaging standard.
A practical release flow is:
- Confirm the governing model, drawing, material, quantity, and finish.
- Produce the prototype or first article using the proposed route where practical.
- Verify the agreed critical features and records.
- Record approved deviations or required changes in a controlled revision.
- Obtain buyer approval for the defined release package.
- Establish in-process checks for characteristics affected by tool wear or setup drift.
- Confirm final inspection, identification, protection, and packaging.
- Retain the approved requirement set for repeat orders.
If a prototype was produced by a temporary route, different material, substitute finish, or reduced inspection plan, do not assume the batch process is automatically validated. Identify what changes in production and whether another first article or partial revalidation is required. The prototype CNC machining services page is relevant when the immediate objective is design, fit, or assembly validation.
13. How Should Drawing Revisions and Engineering Changes Be Controlled?
Every engineering change should be tied to a unique revision and communicated before affected material or production is released. Reusing the same filename without a new revision identifier is not enough because the supplier may not know which dimensions, tolerances, notes, or model features changed.
For each change:
- Issue a new revision identifier and date
- Identify changed dimensions, tolerances, datums, material, finish, notes, or packaging
- Confirm whether open quotations remain valid
- Review the effect on purchased material, work in progress, finished inventory, tooling, gauges, and inspection programs
- State whether a new prototype, first article, or partial validation is required
- Withdraw obsolete files from active production use
- Confirm which revision appears on inspection reports, labels, and packaging
If the previous order included an approved deviation, clarify whether it applies again. Repeat orders should reference the exact released revision and approved exceptions rather than asking for “the same as last time.” A controlled revision history reduces the risk of making a technically correct part to an obsolete requirement.
14. What Determines Price, MOQ, and Lead Time for Precision CNC Turning Services?
Price, minimum order quantity, and lead time are project-specific because they depend on the complete manufacturing and acceptance route. LuckyHXS does not apply one universal MOQ, price, prototype schedule, or batch lead-time promise to every turned part; these items are confirmed after drawing review.
Important variables include:
- Material grade, condition, diameter, stock form, availability, and purchase lot
- Part size, material-removal volume, cutoff loss, and bar utilization
- Thin walls, long slender geometry, deep bores, small tools, and difficult access
- Critical fits, runout, threads, grooves, surface texture, and cosmetic requirements
- Number of setups and off-axis operations
- Special tooling, collets, soft jaws, fixtures, form tools, or gauges
- Heat treatment, plating, anodizing, polishing, grinding, cleaning, or passivation
- Prototype approval, inspection frequency, reports, and material or process documents
- Order quantity, repeat demand, revision stability, and forecast information
- Packaging, destination, shipping method, and required receipt date
Ask the supplier to separate one-time charges from unit price and identify assumptions and exclusions. Request price breaks for several quantities using the same controlled revision. Lead time should state its start event and dependencies, including requirement approval, material, tooling, prototype, buyer approval, batch machining, outside processing, documentation, packaging, and shipment. The article on CNC machining lead time explains why schedules change from project to project.
15. What Should a Complete CNC Turning Quotation Confirm?
A complete quotation should define the finished deliverable and its acceptance basis clearly enough that competing offers can be compared on the same scope. Unit price alone cannot show whether material, secondary operations, finishing, inspection, documentation, packaging, and freight assumptions are equivalent.
Before purchase-order release, confirm:
- Part number, drawing revision, and governing files
- Material grade, condition, stock form, and required material evidence
- Quantity, price breaks, one-time charges, and quotation validity
- Proposed turning route, setups, and included secondary operations
- Included finish, heat treatment, masking, cleaning, and outside processes
- Critical tolerances or features requiring specific capability confirmation
- First-article, in-process, final-inspection, and sampling requirements
- Inspection report, material, finish, or compliance documents included
- Approved deviations, open technical questions, and buyer decisions still required
- Packaging, part identification, delivery basis, destination, and schedule start event
- Tooling or gauge ownership, storage, and reuse where project-specific equipment is charged
- Change-control method for revisions after order release
Resolve contradictions in writing before production. If a quotation says “to drawing,” make sure the supplier received the same current drawing and model that the purchase order references. If the quote excludes a characteristic, report, finish, or secondary operation, decide whether the exclusion is acceptable before comparing price.
Request a Precision CNC Turning Review
Send LuckyHXS your current 2D drawing and matching 3D model, or an approved sample with clear reconstruction and acceptance instructions. Include the exact material, quantities, critical fits and datums, threads and grooves, off-axis features, final finish, inspection records, packaging needs, destination, and required date. Request written confirmation of the proposed process route, finished scope, tolerance feasibility, inspection evidence, quotation assumptions, order quantity, and schedule before production.